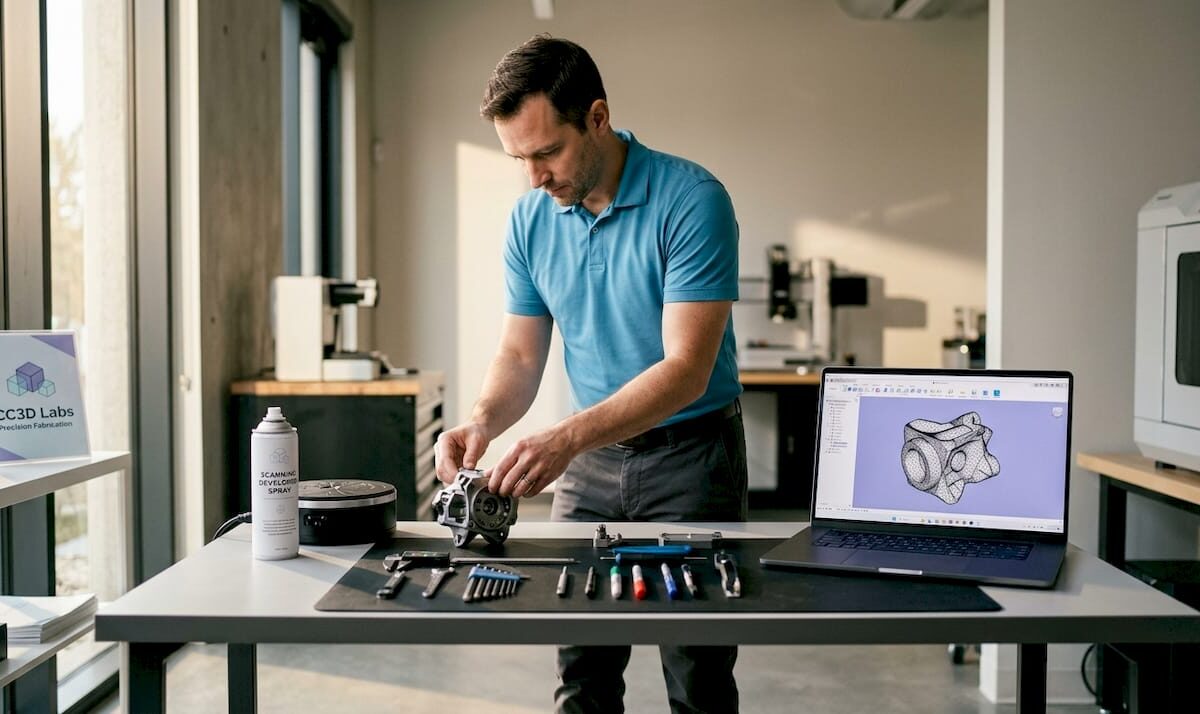
Technician preparing object for 3D scanning in workspace

How to Optimize 3D Scan Accuracy for Better Results


TL;DR:

  • Achieving precise and consistent 3D scan data requires thorough object preparation, appropriate scanner selection, and deliberate environmental control. Techniques like multi-angle scanning, slow overlapping passes, and real-time coverage checks significantly improve accuracy. Post-processing, including careful alignment, noise removal, and validation against references, is essential for producing reliable models.

Getting consistent, precise data from a 3D scanner is harder than the product demos make it look. Whether you’re capturing a machined part for reverse engineering, scanning an organic form for product development, or working up a prototype at home, knowing how to optimize 3D scan accuracy separates usable data from a frustrating rebuild. Incomplete geometry, surface noise, and misaligned point clouds are not hardware problems — they’re technique problems. This guide covers every phase from object prep through post-processing so you can get it right the first time.

Table of Contents

Key Takeaways

Point Details
Prepare surfaces before scanning Apply matte spray to reflective or dark objects to significantly improve point cloud quality.
Multi-angle scanning closes data gaps Scanning horizontally and vertically captures crevices and undercuts a single pass will miss.
Slow, overlapping movement is non-negotiable Erratic scanner movement causes tracking loss and leaves data holes that are hard to repair later.
Post-processing must be methodical Align, then clean noise, then fill holes in that order to avoid compounding errors in your mesh.
Verify accuracy against a reference Compare your scan output against physical measurements or a CAD model before committing to production.

How to optimize 3D scan accuracy before you start

Most accuracy problems are baked in before the scanner ever powers on. Preparation is where you make or break the final result, and it deserves more attention than most guides give it.

Surface treatment comes first. Objects with reflective, transparent, or very dark surfaces frequently require matte spray to improve scan fidelity. Structured light and photogrammetry-based scanners rely on reading surface texture and light patterns. A polished aluminum bracket or a black rubber gasket gives the sensor almost nothing to work with, producing sparse, noisy point clouds. A quick coat of removable scanning spray gives those surfaces the diffuse reflectivity they need.

Match your scanner to the object. A long-range LiDAR unit designed for architectural capture will not resolve the fine features of a 30mm mechanical component. Conversely, a close-range structured light scanner with a small field of view will lose tracking on a large enclosure. Before you scan, confirm your scanner’s rated accuracy, resolution, and working distance are appropriate for the object’s size and the level of detail you need to capture.
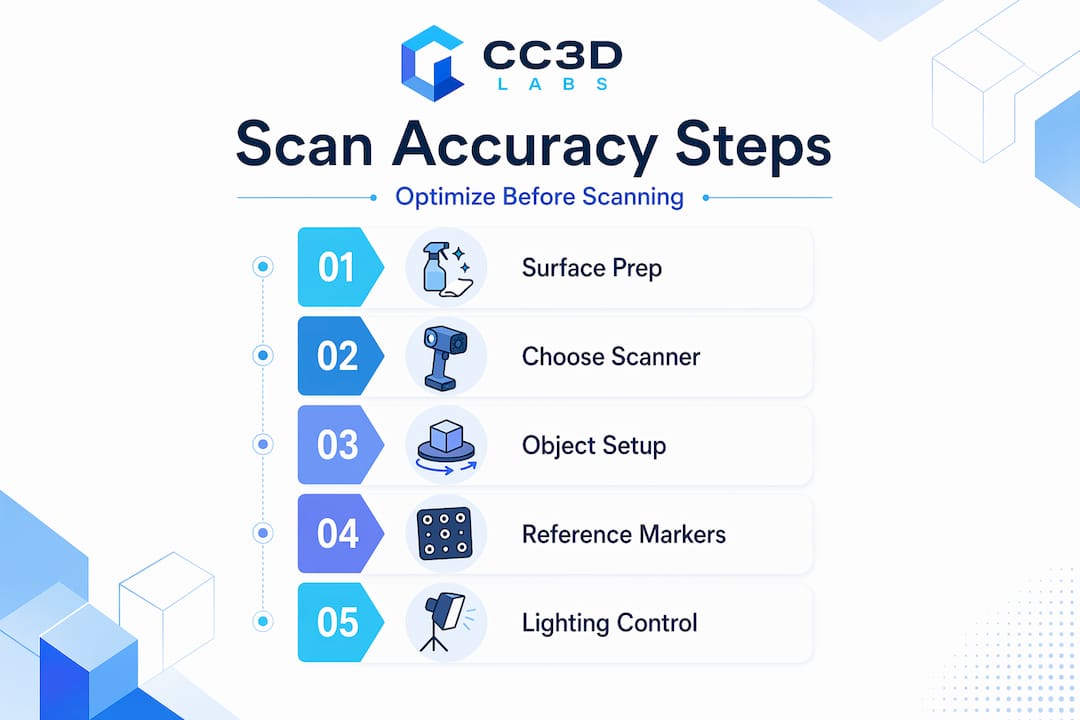
Infographic showing five steps to optimize 3D scan accuracy

Control your environment deliberately. Harsh shadows and direct sunlight cause errors and reduce model fidelity in ways that post-processing cannot fully recover. Set up in a space with soft, diffuse lighting. Overcast daylight works well outdoors. Indoors, use diffused studio lights or even translucent panels over standard fixtures. Avoid scanning near windows with strong directional sun.

Here’s a pre-scan checklist worth running through every time:

  • Clean the object of dust, grease, and fingerprints
  • Apply scanning spray to reflective, transparent, or very dark areas
  • Stabilize the object on a turntable or non-slip mat so it cannot shift mid-scan
  • Confirm ambient lighting is soft and consistent from all angles
  • Check that the scanner is fully warmed up and recently calibrated

Pro Tip: Place your object on a lazy Susan turntable with reference markers printed on the mat underneath. The scanner tracks the markers while you rotate the object, giving you automatic alignment across passes without any repositioning guesswork.

Step-by-step scanning techniques for better precision

With prep complete, what you do during the scan determines how much cleanup you create for yourself afterward. These techniques directly support improving 3D scanning precision.

  1. Move slowly and use overlapping passes. Slow, steady movement with overlapping passes prevents tracking loss and gaps in data. A general rule: each new pass should share at least 30% overlap with the previous one. Think of it like mowing a lawn rather than driving across a field.

  2. Alternate between horizontal and vertical scanner orientations. Rotating the scanner vertically reveals hidden crevices and undercuts that horizontal scanning misses entirely. This is one of the most underused techniques for capturing complex objects. Run a full horizontal pass, then tilt the scanner 90 degrees and make a dedicated vertical pass over any concave areas, threads, or slots.

  3. Apply markers to challenging or symmetrical surfaces. Markers improve scan stability and reduce tracking loss for objects with uniform color, repetitive geometry, or large featureless flat sections. Stick retro-reflective targets in irregular patterns across the object’s surface. The scanner uses these as fixed reference points when natural texture is insufficient.

  4. Adjust exposure and resolution settings for each object. A shiny metallic surface needs lower exposure than a matte plastic part to avoid overblown returns. Reduce resolution slightly on large, simple forms to keep file sizes manageable. Max out resolution only when fine surface detail genuinely matters for your downstream workflow.

  5. Scan from multiple orientations to ensure full coverage. Combining scans from different positions produces more complete coverage of hard-to-reach areas. For most freeform objects, plan for at least three to five distinct scan positions: top, front, back, and both sides at minimum.

  6. Monitor tracking feedback in real time. Most scanning software shows a live tracking indicator. If it starts to drop, stop and back up slightly rather than pushing forward. Recovering lost tracking mid-scan is almost always cleaner than trying to repair the resulting gap in post.

Pro Tip: For symmetrical objects like cylindrical parts or spherical housings, break the symmetry artificially by taping a small piece of masking tape in an irregular position. This gives the scanner a unique reference point to track across the full rotation.

Post-processing best practices for accurate models

Raw scan data is never the finished product. The post-processing phase is where you turn a rough point cloud into a dimensionally accurate mesh, and how you approach it matters as much as the scan itself.
Engineer post-processing 3D scan model on computer

Align before you clean. When working with multiple scan passes, register and align all scans first before touching noise removal or mesh operations. Trying to merge passes after you’ve already modified one of them creates mismatches that can be nearly impossible to reconcile.

Post-processing steps like noise removal, mesh alignment, and hole filling are critical to preserving model accuracy. The order matters:

  • Alignment and registration. Use your software’s global registration function after doing a rough initial alignment. Software with advanced point cloud registration can significantly improve results, particularly when scans have limited overlap. Displacement-corrected geometric consistency algorithms are now making their way into commercial tools and dramatically improve reliability in low-overlap conditions.
  • Noise and outlier removal. Use statistical outlier filters with conservative settings. Aggressive noise removal destroys fine surface detail. Run the filter once at low strength, then visually inspect before applying again.
  • Hole filling and mesh repair. Fill small holes automatically, but handle large holes manually. Automated tools will often interpolate surface curvature incorrectly across wide gaps, creating geometry that was never actually scanned.
  • Export format selection. Export in formats appropriate to your workflow. OBJ and STL are standard for 3D printing and CAD import. PLY retains color and per-point metadata if you need it for inspection or archival. STEP or IGES are better for direct CAD environments when your software supports scan-to-CAD conversion.

Pro Tip: Before you export, run a quick visual inspection by cross-sectioning the mesh in your software. Slicing through the model at several planes reveals internal voids, duplicate geometry, and inverted normals that won’t be obvious from the outside.

Common mistakes that compromise scan accuracy

Even experienced operators repeat these errors. Knowing what to watch for saves you a full rescan.

  1. Ignoring environmental factors. Environmental vibrations, temperature swings, or air movement degrade scan quality by introducing noise and tracking errors. A large HVAC unit cycling on and off near your scan table is enough to introduce measurable error over a long scan session. Scan in a stable, quiet environment whenever precision is critical.

  2. Scanning too fast. Speed feels productive but erratic or rapid movements cause incomplete or misaligned scan passes. The scanner needs time to process and register each frame. Double the time you think you need for any object with complex geometry.

  3. Skipping regular calibration. Skipping calibration leads to inaccurate dimensions and misaligned scans, especially in engineering applications where tolerances are tight. Calibrate at the start of each session, after transport, and any time the scanner has been exposed to significant temperature change.

  4. Not checking coverage in real time. On-site quality checks during scanning reduce rework and improve model completeness. Discovering a missing area when you’re back at your desk means setting up the whole scan again. Spend 30 seconds reviewing coverage before you move the object.

“The single most expensive mistake in 3D scanning is assuming you got it. Verify before you move anything.” This is worth repeating every time you scan a critical part.

Verification methods that confirm scan accuracy

Producing a mesh is not the same as producing an accurate mesh. These techniques help you know which one you have.

Verification method What it checks When to use it
Physical measurement comparison Key dimensions against calipers or CMM data Before any manufacturing commitment
CAD overlay deviation map Color-coded deviation between scan and CAD Reverse engineering and inspection workflows
Point cloud overlap analysis Percentage of coverage and alignment error After merging multiple scan passes
Reference target residuals Error values from marker-based alignment Whenever markers are used during scanning

For high-stakes applications, compare your scan against a physical measurement reference at multiple checkpoints, not just the overall bounding dimensions. A scan can look dimensionally correct at the extremes while carrying localized errors in complex features. CAD overlay tools in software like Geomagic or Polyworks generate heat maps that visualize exactly where deviation is occurring and by how much.

Advanced algorithms like displacement-corrected geometric consistency significantly improve point cloud registration accuracy, particularly in low-overlap conditions. If your scanning software has registration quality scoring, pay attention to it. A high alignment error at the merge stage means your final model carries that error everywhere downstream.

Pro Tip: Scan a known reference object, such as a calibrated sphere or gauge block, at the start of each session. Measure it in software and compare to its certified dimensions. This gives you a real-world accuracy baseline for that specific scan session, not just the manufacturer’s spec sheet.

My honest take on mastering 3D scan accuracy

In my experience, the biggest gap between mediocre scans and exceptional ones is not hardware. I’ve watched engineers with top-tier scanners produce unusable data because they were in a hurry, and I’ve seen hobbyists with mid-range units capture engineering-grade geometry because they were patient and methodical.

Real-time verification changed how I work. I used to finish a full scan session and find missing coverage back at the workstation. Now I treat verification as part of the scanning workflow, not a step after it. That single habit cut my rescan rate dramatically.

The other thing I’ve learned: multi-angle scanning is not optional on anything with undercuts, threads, or deep pockets. A single-pass horizontal scan of a threaded housing looks complete until you try to use the mesh and realize all the thread geometry is missing. Adding a dedicated vertical pass takes five extra minutes and saves an hour of repair work.

The myth I push back on hardest is that a better scanner solves accuracy problems. It doesn’t. Technique, environment, and patience solve accuracy problems. The scanner is just the measurement tool. How you use it determines everything.

Get professional-grade 3D scanning and printing with Cc3dlabs
https://cc3dlabs.com

If you’re working on a project where accuracy genuinely matters, whether it’s a functional prototype, a reverse-engineered component, or a production part series, the DIY path has real limits. Cc3dlabs offers professional handheld 3D scanning (accuracy to ~0.1 mm) services alongside full-cycle 3D printing for engineers and product developers who need results they can trust. The team near Philadelphia handles everything from scan capture through final print, so your data quality is validated at every step. You can also explore the scanning accuracy checklist on the site to cross-reference your current workflow against professional standards. Get a free estimate online or reach out directly if you have a complex part that’s been giving you trouble.

FAQ

What causes poor accuracy in 3D scans?

Poor accuracy most often comes from environmental issues, surface conditions, and scanning technique rather than hardware. Reflective surfaces, harsh lighting, rapid scanner movement, and skipped calibration are the leading causes.

How many scan passes do I need for a complete model?

Most objects require at least three to five distinct scan orientations to achieve full coverage. Complex parts with undercuts, crevices, or internal features need more, and a dedicated vertical-orientation pass is often required.

Do I need scanning spray for every object?

Not every object needs it, but any surface that is highly reflective, transparent, or very dark should be treated. These surface types cause sparse or noisy point clouds that are difficult to repair in post-processing.

How often should I calibrate my 3D scanner?

Calibrate at the start of every scan session, after transporting the scanner, and after any significant temperature change. Skipping calibration introduces dimensional drift that accumulates across a session.

What file format should I export for engineering use?

OBJ and STL work well for most 3D printing applications. For CAD integration and inspection workflows, STEP or IGES formats preserve geometric data more reliably when your software supports scan-to-CAD conversion.
3D modeler working in bright studio

What Is Advanced 3D Modeling: Techniques and Applications


TL;DR:

  • Advanced 3D modeling involves precision parametric design, organic sculpting, and AI workflows that ensure models are production-ready. It relies on geometric representations like polygon meshes, NURBS, and parametric constraints to create models that survive manufacturing, animation, and visualization processes. Mastering topology, UV mapping, and hybrid workflows enables professionals to produce high-quality models efficiently across industries.

Advanced 3D modeling is far more than placing shapes on a digital canvas. When you ask what is advanced 3D modeling, the real answer involves precision parametric design, organic sculpting, intelligent topology management, and AI-assisted workflows that together produce models ready for manufacturing, animation, and architectural visualization. At its core, 3D models represent shape, size, and texture through polygon meshes and mathematical surfaces. This article breaks down the techniques, tools, real-world applications, and emerging trends you need to understand if you want to apply advanced modeling skills to serious design and prototyping work.

Table of Contents

Key Takeaways

Point Details
Beyond basic shapes Advanced 3D modeling combines parametric precision, sculpting, and AI workflows rather than simple geometry creation.
Technique diversity matters Professionals merge CAD, NURBS, and freeform sculpting in hybrid workflows to solve complex spatial and artistic problems.
AI assists but does not replace AI tools accelerate base modeling and texturing while skilled artists handle refinement and production standards.
Applications span industries Manufacturing, gaming, architecture, and virtual production all rely on advanced modeling for prototyping and visualization.
Fundamentals drive AI success Mastering topology and UV mapping remains critical even when AI-generated assets enter the pipeline.

What advanced 3D modeling actually means

Most people associate 3D modeling with creating a rough shape and slapping a texture on it. Advanced 3D modeling sits in a completely different category. It is the discipline of constructing digital geometry with intentional precision, structural logic, and production readiness baked into every decision you make from the first polygon to the final export.

The mathematical foundation matters here. Advanced models rely on three primary geometric representations:

  • Polygon meshes: Grids of vertices, edges, and faces that define surface geometry. Fast to render but require careful topology management to deform cleanly and print accurately.
  • NURBS (Non-Uniform Rational B-Splines): Mathematically smooth curves and surfaces used heavily in industrial CAD. They produce watertight, precise geometry ideal for engineering tolerances.
  • Parametric constraints: Rules and relationships embedded in the model so that changing one dimension automatically updates dependent features throughout the entire design.

The gap between basic and advanced 3D modeling is not just about software complexity. It is about whether your model can survive a real production pipeline. An advanced model transfers cleanly between software environments, holds up under manufacturing tolerances, animates without mesh artifacts, and can be iterated without rebuilding from scratch.

Advanced modeling software today covers a spectrum from parametric CAD platforms to freeform sculpting environments. Each serves a different purpose, and understanding when to use which is part of what separates professionals from beginners. AI’s emerging role in this field is shifting artists from manual geometry creation toward high-level prompt engineering and iterative refinement, but the underlying principles of good modeling have not changed.

Pro Tip: If you are evaluating whether your modeling skills qualify as “advanced,” ask yourself this: can your models survive a file format conversion, a topology audit, and a manufacturing review without significant rework? If the answer is no, that is your learning roadmap.

Advanced 3D modeling techniques and workflows

The techniques that define professional-grade advanced 3D modeling are not learned in isolation. They layer on top of each other in workflows that combine structure, detail, and artistic expression. Here is how the major techniques build on each other in practice:

  1. Parametric modeling. You define geometry through constraints and relationships rather than direct manipulation. Change the wall thickness of a housing component and every connected feature updates automatically. This is the backbone of product design and engineering work, where parametric and generative design solve spatial problems with precision rather than aesthetic guesswork.

  2. Freeform sculpting. Digital sculpting tools let you manipulate virtual clay-like geometry using symmetry, layers, and dynamic remeshing. The priority at this stage is artistic freedom before technical constraints. Characters, organic products, and architectural details all benefit from sculpting workflows that capture nuance no parametric tool can match.

  3. Hybrid CAD-sculpt integration. This is where advanced workflows get genuinely complex. Hybrid workflows use CAD for structural precision and sculpting tools for high-detail organic surfaces, requiring careful translation between NURBS and polygon mesh formats. A product designer might build the structural shell in a CAD environment, export to a sculpting tool for surface detailing, and then retopologize before returning to CAD for final manufacturing prep.

  4. Topology and UV mapping. Clean topology means your mesh deforms predictably for animation and prints without internal geometry conflicts. UV mapping unfolds the 3D surface into a 2D space so textures apply correctly without stretching. These two disciplines are unglamorous but are the difference between a model that works and one that causes problems downstream.

  5. Texture baking and iterative refinement. Baking transfers high-resolution surface detail from a dense sculpt onto a lighter mesh, preserving visual quality without the polygon count that would slow rendering or fail in a game engine. Iterative refinement means reviewing the model at each stage, catching problems before they compound.

Pro Tip: Learn retopology before you need it urgently. Most professionals wish they had learned proper edge flow earlier. Bad topology is the most common reason a client’s model gets rejected at the manufacturing or rigging stage.

AI tools are now entering every step of this workflow. AI-assisted features like automated retopology and intelligent mesh deformation compress timelines significantly. Tools like Meshy.ai produce multiple model variations rapidly for stylized and mid-polygon assets, making iteration faster than ever for the right project types.

Designer using AI retopology tools on 3D mesh

Benefits and practical applications

Understanding the benefits of advanced 3D modeling is straightforward once you see where it connects to real project outcomes. Advanced modeling is not a luxury skill. It is how serious design and manufacturing work gets done.

Here is where the practical value shows up most clearly:

  • Product prototyping. Advanced modeling improves manufacturing and design processes by enabling precise, adaptable, high-fidelity models. Instead of discovering a fit problem during physical assembly, you catch it in the parametric model and update the design in minutes.
  • Architecture and spatial design. Architects using parametric tools can test structural configurations and aesthetic variations within the same model file, reducing costly design revisions. Digital tools in construction can reduce project costs measurably when modeling accuracy drives early-stage decisions.
  • Gaming and virtual production. Character artists combine sculpting for hero detail and retopology for real-time game engines. The same pipeline feeds into virtual production environments where physical accuracy and visual fidelity both matter.
  • Manufacturing visualization. Engineers use advanced 3D models to simulate assembly sequences, stress test components virtually, and communicate design intent across global teams before a single physical part is produced.
Application Area Primary Modeling Approach Key Benefit
Product design Parametric CAD Precise tolerances, fast iteration
Character and creature art Freeform sculpting Organic detail, artistic control
Architecture Hybrid parametric and mesh Spatial problem solving, visualization
3D printing and prototyping CAD to mesh pipeline Printable geometry, manufacturing accuracy
Gaming and real-time environments Retopologized sculpts Optimized poly count, clean deformation

The creative freedom argument is real too. Sculpting gives artists control that box-modeling never could. But the most powerful outcome of advanced 3D modeling is speed with quality. When your workflow is solid, you can go from concept to print-ready or render-ready file faster than any earlier generation of designers.

Challenges and what comes next

Advanced 3D modeling is not a skill you pick up over a weekend. The challenges are genuine, and the field is changing fast enough that even experienced modelers need to keep adapting.

The persistent technical challenges include:

  • Topology cleanup. AI-generated models often require significant retopology before they are production ready. Post-generation cleanup includes retopology and fixing non-manifold geometry to ensure compatibility with rendering engines and 3D printing workflows.
  • Format interoperability. Moving models between CAD, sculpting, and rendering environments often introduces data loss or geometry errors. Managing NURBS and polygon meshes without losing design intent is one of the most technically demanding aspects of hybrid workflows.
  • Skill gaps in texture pipelines. Junior artists often need mentorship to master topology, UV mapping, and texture pipelines even when they are working with advanced software. The tools do not teach the judgment.

“AI effectively lowers the skill floor and compresses timelines significantly, but the ceiling is still defined by the human who refines and directs the work.”

Looking forward, the field is moving toward real-time sculpting in collaborative cloud environments, spatial computing interfaces that let designers manipulate geometry physically, and AI that can handle increasingly complex base model generation. The artists who will succeed are those treating AI as a skilled collaborator rather than a replacement for foundational knowledge.

My take on mastering advanced 3D modeling in 2026

Infographic showing main steps in advanced 3D modeling workflow

I have watched a lot of people approach advanced 3D modeling the same way. They jump to the most sophisticated software they can find, spend weeks learning its interface, and then produce work that falls apart the moment a client needs it to be printable or rigged. What I have learned is that the fundamentals are not the boring part. They are the part that makes everything else possible.

The most capable modelers I know are not the ones who adopted AI tools first. They are the ones who understand why topology flows a certain way, what happens when geometry is non-manifold, and how UV seams affect texture quality. Because they understand those things, they can direct AI tools effectively and fix what the automation gets wrong. My honest advice: spend real time on topology, spend real time on the math behind your surfaces, and then let AI speed up the work you already understand. The 3D modeling and CAD project gallery at Cc3dlabs is a good place to see what production-ready advanced modeling actually looks like in practice.

— Justin

Turn your advanced models into physical reality with Cc3dlabs

https://cc3dlabs.com

Advanced 3D modeling is where precision design begins. But the real test of any model is whether it survives contact with the physical world. Cc3dlabs, located near Philadelphia, works directly with designers, engineers, and product developers to take advanced 3D models through to high-quality printed parts. Their 3D printing services cover everything from single prototypes to batch production runs, with filament-based printing capable of meeting tight tolerances for functional parts. They also offer professional handheld 3D scanning (accuracy to ~0.1 mm), which feeds directly into advanced modeling workflows when you need to capture existing geometry accurately. If you are ready to validate your design in the real world, Cc3dlabs offers free online estimates and local pickup for Philadelphia-area clients.

FAQ

What is advanced 3D modeling?

Advanced 3D modeling is the practice of creating production-ready 3D geometry using parametric constraints, freeform sculpting, and topology management techniques that go beyond basic shape creation. It encompasses both CAD-driven precision and artistic sculpting workflows, often combined in hybrid pipelines.

How is advanced 3D modeling different from basic 3D modeling?

Basic 3D modeling produces simple geometry for visualization purposes. Advanced 3D modeling produces models with clean topology, accurate tolerances, proper UV mapping, and the structural integrity needed for animation, manufacturing, or 3D printing.

What software is used for advanced 3D modeling?

Professionals use a range of advanced modeling software depending on the application, including parametric CAD platforms for engineering and sculpting tools for organic design. Many advanced workflows combine multiple software environments, translating between NURBS-based and polygon-based geometry.

How does AI fit into advanced 3D modeling workflows?

AI tools generate base models and automate tasks like retopology and mesh deformation, but post-generation cleanup is still required for production-ready assets. AI shifts the artist’s role toward high-level direction and refinement rather than eliminating the need for technical skill.

How do I learn advanced 3D modeling?

Start by building a strong foundation in topology, UV mapping, and at least one parametric CAD platform. Then layer in sculpting tools and hybrid workflows. Working with real production constraints, such as preparing models for 3D printing, accelerates learning faster than purely artistic projects.

Engineer inspecting 3D printed part at workbench

The Role of Part Validation in 3D Printing for Manufacturers


TL;DR:

  • Part validation in 3D printing ensures a process consistently produces conforming parts, not just individual successful prints.
  • Implementing structured IQ/OQ/PQ procedures and using multiple validation techniques reduces scrap, enhances quality, and meets regulatory standards.

Most manufacturers assume that once a 3D printer finishes a job, the part is ready to use. That assumption is expensive. The role of part validation in 3D printing is far more critical than most production teams realize, and the gap between “it printed” and “it works reliably” is where quality problems, warranty failures, and regulatory risks pile up. Projects that skip validation show 3 to 5 times higher scrap rates in the first three months of production. This article breaks down what validation actually involves, which techniques work, and how to build a process that protects your parts and your bottom line.

Table of Contents

Key takeaways

Point Details
Validation goes beyond inspection Process validation confirms repeatable results across all future builds, not just one good part.
Multiple techniques compound accuracy Combining dimensional checks, 3D scanning, and functional testing catches defects that single-method inspection misses.
Business impact is measurable Proper validation dramatically reduces scrap, rework costs, and machine downtime across production runs.
Regulated industries require it Medical, aerospace, and defense applications mandate formal IQ/OQ/PQ validation before production parts ship.
Continuous monitoring sustains quality SPC systems fed by validation data catch process drift before it becomes a defect wave.

The role of part validation in 3D printing explained

Part validation and product inspection are not the same thing, and confusing the two is one of the most common mistakes manufacturers make when scaling from prototype to production. Inspection checks whether a specific part meets specifications. Validation proves that the process consistently produces conforming parts within defined parameters, every time, without relying on 100% inspection to catch failures.

Think of it this way: inspecting one part from a batch of 500 tells you about that one part. Validating the process tells you whether all 500 are likely to be good before you even measure them.

Infographic showing steps in 3D print part validation

In regulated industries, this distinction carries legal weight. Process validation is mandatory for medical devices, aerospace components, and pharmaceutical manufacturing equipment. Regulatory bodies require documented evidence that the process, not just the product, is under control. But even outside those industries, validation is the framework that separates reactive quality control from proactive quality assurance.

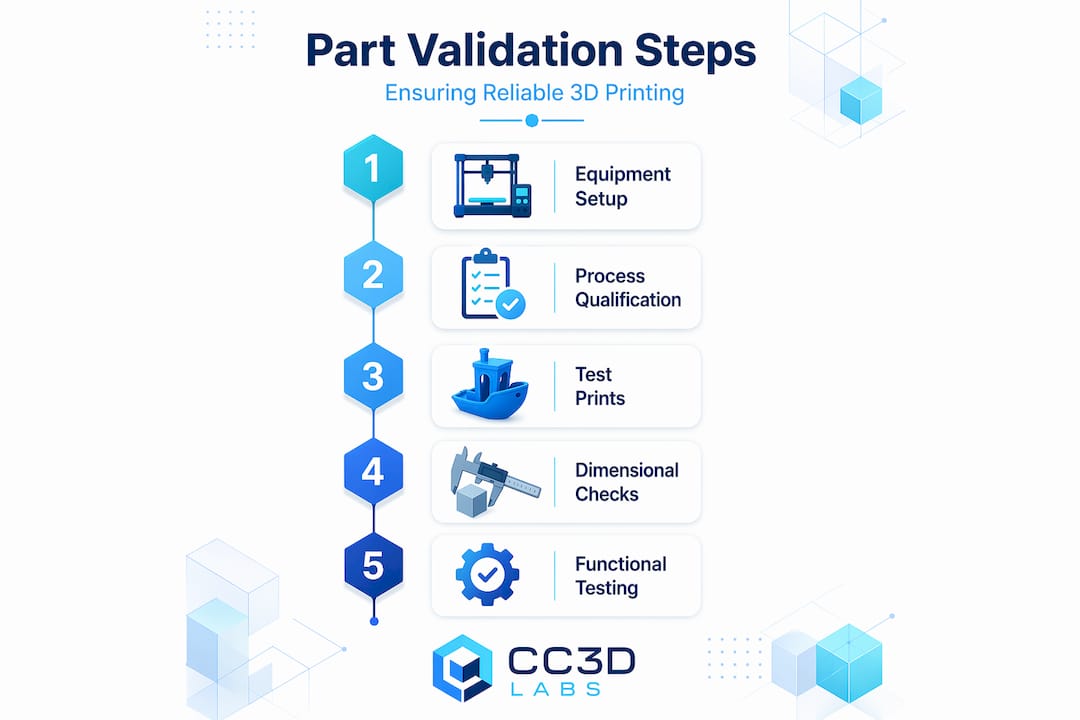
The most widely adopted framework is IQ/OQ/PQ, adapted directly from pharmaceutical and medical device manufacturing:

  • Installation Qualification (IQ): Confirms the printer and supporting equipment are installed correctly, calibrated, and operating within manufacturer specifications.
  • Operational Qualification (OQ): Tests whether the process produces conforming parts across the defined operating range, including edge conditions.
  • Performance Qualification (PQ): Demonstrates that the validated process consistently delivers acceptable output under real production conditions over time.

Equipment qualification follows this IQ to OQ to PQ sequence as a prerequisite to process validation, and skipping any stage undermines the entire framework. This structure forces manufacturers to think systematically rather than relying on operator intuition.

Pro Tip: When starting a validation program for 3D printing, document your IQ stage meticulously. Calibration records, environmental conditions, and software version logs protect you during audits and give you a meaningful baseline when troubleshooting future deviations.

Methods for part validation that actually work

Choosing the right validation technique depends on part geometry, material, application criticality, and whether you need destructive or non-destructive data. Most production environments benefit from layering multiple approaches rather than relying on any single method.

Dimensional measurement and 3D scanning

Calipers and coordinate measuring machines (CMMs) remain reliable for straightforward geometries. However, for complex organic shapes, thin walls, or surfaces that require full-field data, structured-light or laser 3D scanning delivers far more information per measurement cycle. Aerospace manufacturers illustrate the scale of this advantage: Boeing has publicly described AI-assisted validation tooling that saves hours of inspection time per aircraft.com/news/how-boeing-is-using-ai-for-rapid-parts-validation/” rel=”nofollow noopener noreferrer” target=”_blank”>AI-powered validation tool saves 17 or more hours per aircraft during inspection, while reducing gauge repeatability and reproducibility variance to 0.93%. That level of measurement consistency would be impossible with manual methods alone.

Functional and mechanical testing

Dimensional accuracy tells you if a part is shaped correctly. Functional testing tells you if it performs correctly under load, temperature, chemical exposure, or repeated cycling. For structural components, this might mean tensile or compression testing. For enclosures, it might mean IP rating validation. Destructive testing is sometimes the only honest way to understand failure modes, particularly for safety-critical parts where the cost of a field failure far exceeds the cost of the test sample.

Statistical process control and capability metrics

  1. Collect baseline data across multiple print runs using consistent measurement methods and operator protocols.
  2. Calculate Cpk and Ppk to quantify how well the process holds critical dimensions within specification limits.
  3. Set up control charts for key process variables like nozzle temperature, layer adhesion, and print speed.
  4. Establish control limits based on your baseline and trigger revalidation when measurements drift outside them.
  5. Feed data back into your process settings to tighten variation over time.

Validation data integrates directly with SPC systems for early detection of variation and continuous process improvement. This transforms validation from a one-time event into an ongoing quality intelligence system.

Pro Tip: Do not target a Cpk of exactly 1.0 when setting your process capability goals. Aim for 1.33 or higher. That margin gives your process room to drift before parts fall out of spec, which means fewer emergency stops and more predictable output.

A comparison of common validation techniques by application:

Technique Best for Destructive? Cost level
CMM dimensional inspection Prismatic, tight-tolerance parts No Medium
Structured-light 3D scanning Complex geometry, full-field data No Medium to high
Tensile and compression testing Structural or load-bearing parts Yes Low to medium
CT scanning Internal features, porosity detection No High
Functional performance testing End-use assemblies, fit checks Sometimes Varies

Learning more about ways to validate 3D designs can help you choose the right combination for your specific production environment.

Business impact of rigorous part validation

The financial argument for validation is not abstract. Filament runout and mid-print failures waste real material and machine time on any print farm, and proper process validation dramatically reduces those losses. That is one failure mode. Multiply it across material inconsistency, temperature variation, and calibration drift, and the cumulative cost of unvalidated 3D printing operations becomes significant.

Manufacturers who build validation into their workflow see measurable improvements across four areas:

  • Scrap and rework reduction: Catching process drift early prevents entire batches from becoming waste. The difference between catching a problem at print cycle 3 versus print cycle 300 is the difference between a minor correction and a production crisis.
  • Customer confidence: Validated parts ship with documented proof of conformance. For product developers sourcing parts from contract manufacturers, this documentation is the difference between an acceptable supplier and a preferred supplier.
  • Regulatory readiness: Companies in medical, aerospace, or defense supply chains cannot bid on regulated contracts without validated processes. Building that infrastructure now opens market doors later.
  • Scalability from prototype to production: A prototype can tolerate variability. A production run cannot. Validation is what makes the transition from “it worked once” to “it works every time.”

Scaling production without validation is like building a house on a foundation you have never tested. It might hold, but you will not know until something fails. A well-documented validation record also reduces engineering review time when design changes trigger revalidation, since your process baseline is already defined.

Challenges in validation and how to address them

Supervisor reviewing production in 3D print facility

Integrating part validation into a 3D printing workflow is not without friction, especially for manufacturers who built their operations around rapid iteration rather than process rigor.

The most persistent challenge is measurement uncertainty. Knowing that a part is within tolerance requires that your measurement system is itself accurate and repeatable. Misaligned mating parts caused by unclear dimensional definitions often trace back to incomplete GD&T on drawings rather than actual process failures. Fixing the drawing is faster and cheaper than retesting the process, but you have to know which problem you are actually solving.

Environmental variability is another overlooked factor. Humidity, ambient temperature, and even vibration from nearby equipment affect print quality in ways that are invisible until validation data reveals the pattern. This is where the distinction between Factory Acceptance Testing and Site Acceptance Testing becomes practical. FAT confirms equipment performance in a controlled environment, while SAT validates that same performance under your actual production conditions. A printer that passes FAT may still behave differently on your shop floor, and SAT validates real-world performance for long-term stability.

Best practices for making validation sustainable:

  • Start with a risk-based sampling plan. Not every part or every batch needs 100% inspection. Identify your highest-risk features and focus measurement resources there.
  • Define revalidation triggers upfront. Material lot changes, nozzle replacements, firmware updates, and facility moves all warrant revalidation. Write them down before production starts.
  • Build documentation habits early. Validation reports are only useful if they reflect what actually happened. Standardize your data capture formats from day one.
  • Treat print accuracy insights as a continuous feedback loop rather than a pass/fail gate at the end of a run.

Pro Tip: If you are launching a validation program with limited resources, start with your most critical dimension on your most common part. Validate that one feature thoroughly, document your results, and build from there. A narrow validation done well is more useful than a broad validation done superficially.

My take on where validation fits in your strategy

I’ve talked with a lot of manufacturers who treat part validation as something you do for auditors. You prove compliance, file the paperwork, and move on. In my experience, that framing costs them more than they realize.

What I’ve seen work is treating validation as a data collection strategy. Every measurement you take, every capability study you run, every batch you document gives you a clearer picture of what your process is actually doing versus what you think it’s doing. The manufacturers who use that data proactively, adjusting parameters before scrap rates climb rather than after, are the ones who scale 3D printing production without the chaos that typically comes with it.

The other thing I’d push back on is the idea that validation is only for regulated industries. I’ve seen product developers lose significant time and money when a part that worked perfectly in prototyping failed consistently in production, specifically because no one validated the transition. The process that produced five good prototypes is not automatically the same process that will produce five hundred reliable production parts.

Start lean. Start with one part, one critical feature, one documented study. The insights you get from that first real validation run will tell you more about your process than months of informal inspection. And when you’re ready to scale your 3D printing with confidence, you’ll have the data to back every decision.

— Justin

How Cc3dlabs supports your validation needs

Reliable 3D printed parts start with a process built for quality from the first layer to the final inspection. At Cc3dlabs, we bring professional handheld 3D scanning (accuracy to ~0.1 mm), precision filament-based printing, and design support together under one workflow, so product developers and manufacturers get parts they can actually validate.

https://cc3dlabs.com

Whether you need functional prototypes with documented dimensional reports, batch production runs with consistent quality, or scanning services to compare printed parts against CAD geometry, Cc3dlabs has the equipment and experience to back it up. Our 3D printing services are built around the kind of accuracy and repeatability that makes validation straightforward, not a burden. Get a free online estimate today and see how a quality-focused print partner changes what’s possible for your production program.

FAQ

What is part validation in 3D printing?

Part validation in 3D printing is the process of confirming that a print workflow consistently produces parts meeting defined specifications, not just that a single part passed inspection. It focuses on the process, not just the product.

Why do manufacturers skip part validation?

Most manufacturers skip validation because they perceive it as time-consuming or only required for regulated industries. In practice, skipping validation leads to 3 to 5 times higher scrap rates in early production, making it far more costly than the validation itself.

What methods are used for part validation in 3D printing?

Common methods include CMM dimensional inspection, structured-light 3D scanning, functional mechanical testing, CT scanning for internal features, and statistical process control using Cpk metrics to track process capability over time.

How does the IQ/OQ/PQ framework apply to 3D printing?

IQ confirms correct printer installation and calibration, OQ tests the process across its operating range, and PQ demonstrates consistent output under real production conditions. This sequence is a prerequisite for regulatory compliance and is increasingly adopted in non-regulated 3D printing operations as a best practice.

When should a manufacturer revalidate their 3D printing process?

Revalidation is required after material lot changes, equipment repairs or replacements, firmware or software updates, facility moves, and any design changes that affect critical dimensions. Documenting these triggers upfront prevents gaps in your quality record.

3D designer working on office CAD workstation

3D modeling process for businesses: a step-by-step guide


TL;DR:

  • Flawed 3D models incur high costs and delays when errors are discovered late in manufacturing. Implementing a structured workflow, including validation gates and proper file formats, ensures geometry integrity and reduces rework. An integrated PLM system connects design stages, enabling simultaneous processes and maintaining a single source of truth for efficient product development.

Flawed 3D models are expensive. A geometry error caught after parts are machined can set a product launch back weeks and cost thousands in rework. Yet most manufacturing businesses still treat the 3d modeling process for businesses as an informal, tool-by-tool activity with no standardized handoffs, no validation gates, and no version control. The result is predictable: duplicate revisions, miscommunication between design and manufacturing teams, and prototypes that fail on the first print run. This guide gives you a structured, stage-by-stage workflow to fix that.

Table of Contents

Understanding the 3D modeling workflow for manufacturing businesses

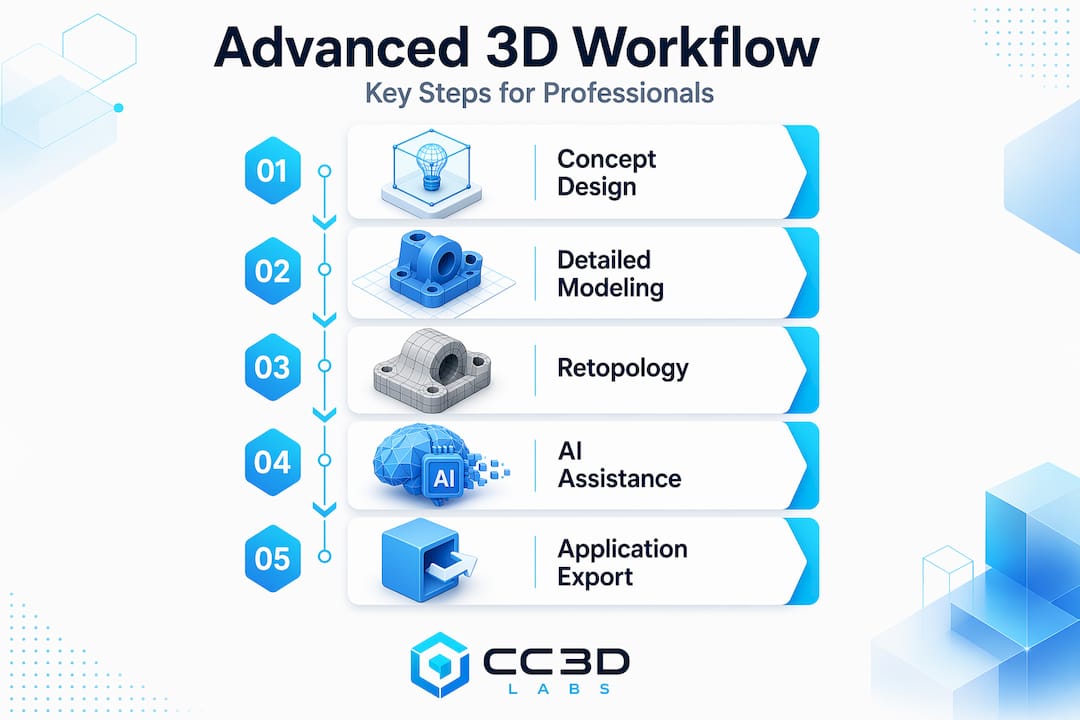
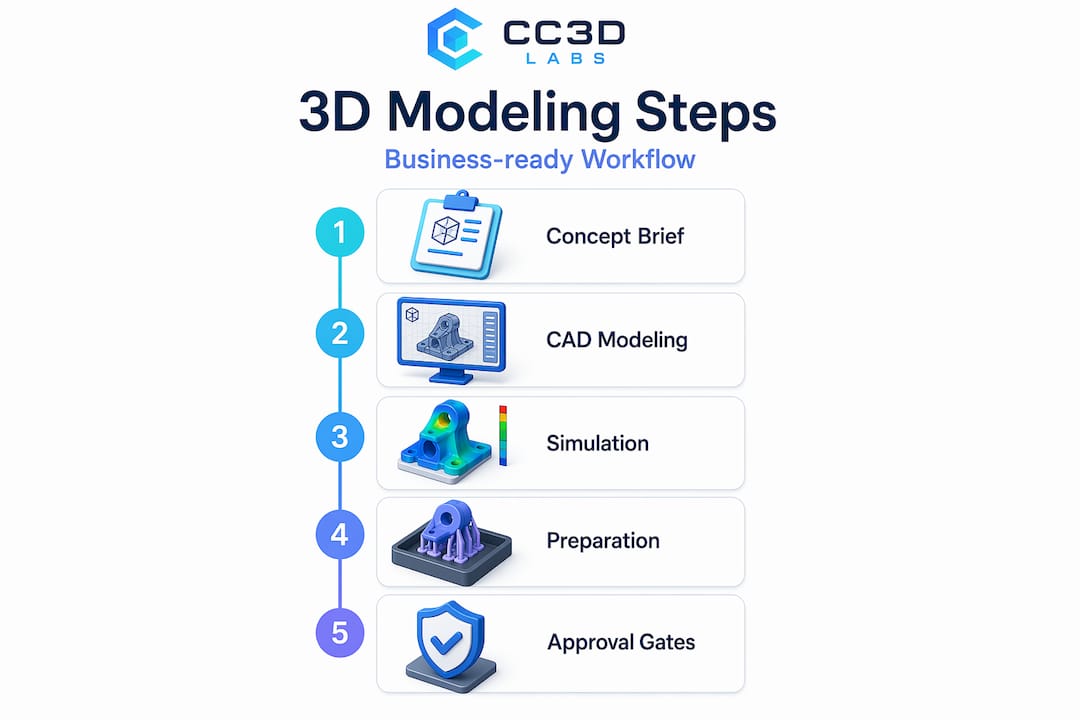
Every reliable product development cycle runs on a defined sequence of stages. The business-ready 3D modeling workflow follows this structure: Concept and brief, CAD geometry design, CAE (computer-aided engineering) simulation and validation, CAM (computer-aided manufacturing) planning, then manufacturing with ERP cost tracking. Product lifecycle management (PLM) sits above all of it as the system of record, connecting every tool and every team.

Without PLM as the connective layer, these stages operate in silos. A CAD designer updates a wall thickness. The CAE analyst runs stress simulations on the old version. The CAM programmer generates toolpaths from a model that no longer exists. That chain of disconnected handoffs is where most manufacturing delays originate.

The five core stages at a glance:

Stage Tool Primary output
Concept and brief Requirements docs, sketches Design intent and constraints
CAD geometry design SOLIDWORKS, Fusion 360, Creo Solid 3D model files
CAE validation ANSYS, Nastran, SimScale Simulation reports
CAM planning Mastercam, HSMWorks Toolpaths and G-code
Manufacturing and cost tracking ERP, PLM Production records and BOM

Infographic with 3D modeling workflow steps

Approval gates between each stage are not bureaucratic overhead. They are cost-control mechanisms. A model that fails CAE validation should never reach CAM programming. Enforcing that boundary through PLM approval workflows eliminates the most expensive class of rework: discovering structural problems after tooling has already been produced.

For businesses scaling toward production, reading a manufacturing-grade 3D printing guide alongside this workflow will clarify how design decisions upstream affect print quality and production yield downstream.

Preparing 3D models for manufacturing: ensuring geometry validity and quality

A valid workflow means nothing if the geometry inside your models is broken. Before any model reaches slicing software or a CNC controller, it must pass two geometric tests: it must be watertight and it must be manifold.

Engineer examining 3D printed part for issues

Watertight means the model has no holes or gaps in its surface. Think of it as a sealed container. If you filled it with water, nothing would leak. Manifold means every edge in the mesh is shared by exactly two faces and no more. These are not cosmetic requirements. A model that fails either condition causes slicer failures including missing layers or infinite calculation loops, because the slicing software cannot determine where the inside of the object begins and ends.

Non-manifold edges and open shells create ambiguous topology, which forces slicers into undefined states. The practical consequences range from incomplete prints to parts with internal voids that only reveal themselves under load testing.

Common geometry problems that cause manufacturing failures:

  • Open shells and gaps at seams between joined bodies
  • Non-manifold edges where three or more faces share one edge
  • Inverted surface normals pointing inward instead of outward
  • Self-intersecting faces that overlap within the mesh
  • Zero-thickness walls generated from Boolean subtractions
  • Duplicate faces at assembly join points

The best time to catch these issues is immediately after modeling, before texturing, rigging, or any downstream processing. Run automated mesh analysis using tools built into your CAD platform or dedicated repair software. Then manually inspect high-risk areas like Boolean unions, imported geometry from external sources, and complex joint intersections.

Pro Tip: Boolean operations (cutting one solid from another) are the single most common source of non-manifold geometry in mechanical CAD. After every Boolean, run a quick geometry check before moving forward. It takes 30 seconds and saves hours.

For a structured approach to validating 3D designs for manufacturing or guidance on designing reliable 3D prints from the ground up, those resources will take you deeper into the practical side of geometry quality.

Choosing the right CAD file formats for your 3D modeling process

Geometry validity matters. File format selection matters just as much, and most businesses get this wrong until a manufacturer sends their file back with a rejection notice.

The two formats you will encounter most often are STEP and STL. They are not interchangeable. STEP files carry full solid geometry and are the preferred format for CNC machining because CAM software needs parametric surface data to generate accurate toolpaths. STL files describe geometry as a mesh of triangles, which is exactly what 3D printing slicers need but is fundamentally incompatible with CNC workflows.

STEP vs. STL: when to use each

Property STEP STL
Geometry type Solid (B-rep) Triangle mesh
Best use case CNC machining, injection molding FDM, SLA, SLS 3D printing
Carries tolerances Yes No
CAM software support Universal Limited
File size Larger Compact

Export best practices to follow every time:

  1. Confirm your model is in the correct unit system (millimeters for most manufacturing) before exporting.
  2. Export individual parts rather than full assemblies unless the manufacturer has explicitly requested an assembly file.
  3. Set STEP export options to AP214 or AP242 for maximum compatibility with downstream CAM systems.
  4. For STL exports, increase the triangle resolution (chord height and angular deviation settings) to reduce faceting on curved surfaces.
  5. Open the exported file in a separate viewer to confirm it looks correct before sending it to a manufacturer.

Pro Tip: Always export a fresh STEP file directly from your finalized CAD model. Never send a STEP that was converted from an STL. That conversion path destroys solid geometry data and produces triangle-mesh pseudo-solids that most CAM software handles poorly.

Understanding the full landscape of CAD file formats for 3D printing is worth the time investment if your team is managing multiple manufacturing processes simultaneously.

Managing 3D model iterations and approvals with PDM workflows

Version control for 3D models is where most small and mid-size manufacturing teams fall behind. Emailing CAD files back and forth, saving versions as “final_v3_REAL_USE_THIS.sldprt,” and losing track of which drawing revision matches which physical prototype are all symptoms of a missing product data management (PDM) system.

SOLIDWORKS PDM tracks design file states, transitions between states, complete version histories, and access permissions. A typical PDM workflow assigns models to states like “In Work,” “Pending Approval,” and “Released.” Transitions between states (like “Submit for Approval” or “Request Change”) require explicit action and generate an audit trail. No one can accidentally overwrite a released drawing.

What a healthy PDM workflow gives your team:

  • A single source of truth for every file revision
  • Clear accountability for who approved which version and when
  • Automatic notifications when a file moves to a new state
  • Controlled access so machinists see only released drawings
  • Rollback capability if a new revision introduces problems

The efficiency gain from PDM is not just organizational. When a design change is made, PDM flags every file that references the modified part, preventing the scenario where a downstream assembly still references the old geometry. That kind of associativity awareness alone eliminates a significant category of rework.

Keep PDM workflows lean. Four to six states are usually enough for a manufacturing business. Overly complex workflows with a dozen transition rules create friction and encourage teams to work around the system entirely.

For a broader look at how file management fits into the 3D modeling workflow, that guide connects the dots between individual modeling decisions and team-wide processes.

Validating and troubleshooting your 3D models before manufacturing

Running geometry checks during modeling is good practice. Running a formal validation pass before releasing a file to manufacturing is non-negotiable.

Topology validation should function as a release gate, blocking files that fail manifold or watertight checks from reaching slicing or machining workflows. That is not an opinion. It is the only approach that prevents bad geometry from causing tool crashes, failed prints, or scrapped parts.

Recommended validation sequence:

  1. Import the model into a validation tool or use your CAD platform’s built-in diagnostics immediately after finalizing geometry.
  2. Run an automated mesh analysis to flag non-manifold edges, open shells, and self-intersections.
  3. Check surface normals. Inverted normals cause inside surfaces to read as outside surfaces in slicers.
  4. Inspect wall thickness across the entire model and compare against the minimum wall requirements for your chosen manufacturing process.
  5. If errors are detected, repair them in the source CAD file and re-export. Never patch errors only in the exported mesh.
  6. Run the validation sequence again after repair. One fix can expose adjacent problems.

Most common errors found at validation:

  • Non-manifold edges at Boolean operation seams
  • Open shells from imported geometry fragments
  • Inverted normals on mirrored bodies
  • Self-intersecting faces from lofts or sweeps with tight radii
  • Zero-thickness walls from coincident face pairs

Validation pipelines that automatically detect and attempt repairs prevent invalid geometry from ever reaching manufacturing. Investing in that automation, even in a simple form, pays for itself on the first avoided print failure.

“Skipping pre-manufacturing validation is the single most predictable cause of prototype delays. The geometry problems were always there. You just chose the most expensive moment to find them.”

For teams aiming for tight tolerances and repeatable results, the 3D print accuracy guide covers the downstream side of what validation protects.

Why integrated PLM workflows are the game-changer for 3D modeling efficiency

Here is what most articles on this topic avoid saying: the individual best practices covered above, geometry checks, file format selection, PDM workflows, only work reliably when they are connected by a system that enforces sequence and propagates change automatically.

The biggest efficiency struggle in 3D modeling is not bad geometry or wrong file formats. It is disconnected handoffs. A CAD team working in isolation from their CAE colleagues will generate structurally valid-looking models that fail simulation. A CAM team working from a stale STEP file will produce toolpaths for a geometry that no longer reflects the approved design. PLM eliminates both failure modes by ensuring every team works from the same design truth, and that every change to the master model propagates automatically to all downstream consumers.

The advantage most businesses miss is that PLM enables parallel workflows rather than sequential ones. CAE stress analysis and CAM toolpath generation can run simultaneously on the same approved model, cutting development time significantly. Sequential handoffs, where CAM waits for CAE to finish, double the schedule risk.

Associativity is the key word here. Every downstream artifact, simulation setup, toolpath, drawing, BOM line, must be associatively linked to the master CAD geometry. When the geometry changes, everything updates. When it does not update, you get what most teams call “mystery failures”: manufactured parts that do not match drawings that do not match the model everyone approved.

The businesses that see the most from 3D modeling investment are not the ones with the most powerful CAD software. They are the ones with disciplined, integrated workflows that treat geometry as a single source of truth rather than a file that gets emailed around. Adopting that mindset, even at the small business level, is what separates teams that prototype once from teams that prototype six times before getting it right.

For practical guidance on making this work at lower production volumes, the low-volume manufacturing tips resource covers how to scale these principles without enterprise-level tooling budgets.

Explore professional 3D modeling and printing services to accelerate your product development

When internal resources become a bottleneck, working with a professional 3D modeling and printing partner can close the gap between design intent and physical prototype faster than most teams expect.

https://cc3dlabs.com

CC 3D Labs, based near Philadelphia, provides 3D printing services and high-accuracy 3D scanning for design accuracy that integrate directly into manufacturing workflows. Whether your team needs a validated CAD model turned into a functional prototype, a batch of production parts, or scan data from an existing component to reverse engineer, CC 3D Labs delivers with fast turnaround and the geometry precision that manufacturing demands. Explore the full range of 3D printing prototypes and parts to see what is possible for your next product development cycle.

Frequently asked questions

What is the role of PLM in the 3D modeling process for businesses?

PLM integrates CAD, CAE, CAM, and ERP tools by managing design versions and approval gates, ensuring all teams work from the same updated models to prevent errors and costly rework. As the system of record above all tools, PLM enforces consistent design truth and controls when models move between workflow stages.

Why must 3D models be watertight and manifold before printing?

Watertight and manifold geometry ensures 3D printers can unambiguously define the object’s volume to generate correct toolpaths. Non-manifold edges cause slicers to fail by producing incorrect toolpaths or entering infinite processing loops.

Which CAD file format is best for CNC machining?

STEP files are the best choice for CNC machining because they contain full solid geometry and are widely supported by CAM systems. STL is mesh-based and suited for 3D printing only, making it incompatible with accurate CNC toolpath generation.

How do PDM workflows improve 3D model management in teams?

PDM systems manage design file states, track versions, and control access with clear workflows like “Submit for Approval” and “Request Change,” reducing confusion and ensuring design integrity. SOLIDWORKS PDM tracks file states and transitions, giving teams a reliable audit trail for every revision.

What are common issues caught during 3D model validation before manufacturing?

Validation detects non-manifold edges, open shells, inverted normals, and self-intersections, all of which cause failures in slicing, machining, or assembly simulations if not fixed early. Validation pipelines catch topology issues automatically, preventing invalid geometry from reaching manufacturing and triggering costly downstream failures.