Small batch FDM parts printing on textured plates

Small Batch FDM Production: A Guide for Engineers

Small-batch FDM production means making real, usable parts in quantities from a handful to a few hundred or more on fused deposition modeling printers, with no mold or tooling cut first. It works best when the part is made of a thermoplastic, fits within roughly 12 inches per side, tolerates ±0.2–0.5 mm, and may still change. At CC 3D Labs, we run a production farm of Bambu Lab FDM printers in Bucks County, PA, and we quote every production job individually after a test print of your actual model, so the batch you approve is the batch you receive.

CC 3D Labs
Move from Prototype to Production
CC 3D Labs produces small-batch FDM parts in Bucks County, with each production job quoted after a test print of your model.

Visit

TL;DR

  • FDM suits batches of roughly 1 to 1,000+ parts that need no tooling, a short time to market and thermoplastic materials. Altair’s FDM production guide gives those same limits.
  • Plan for ±0.2–0.5 mm tolerances on FDM parts, and design around build orientation, wall thickness and supports before you finalize CAD.
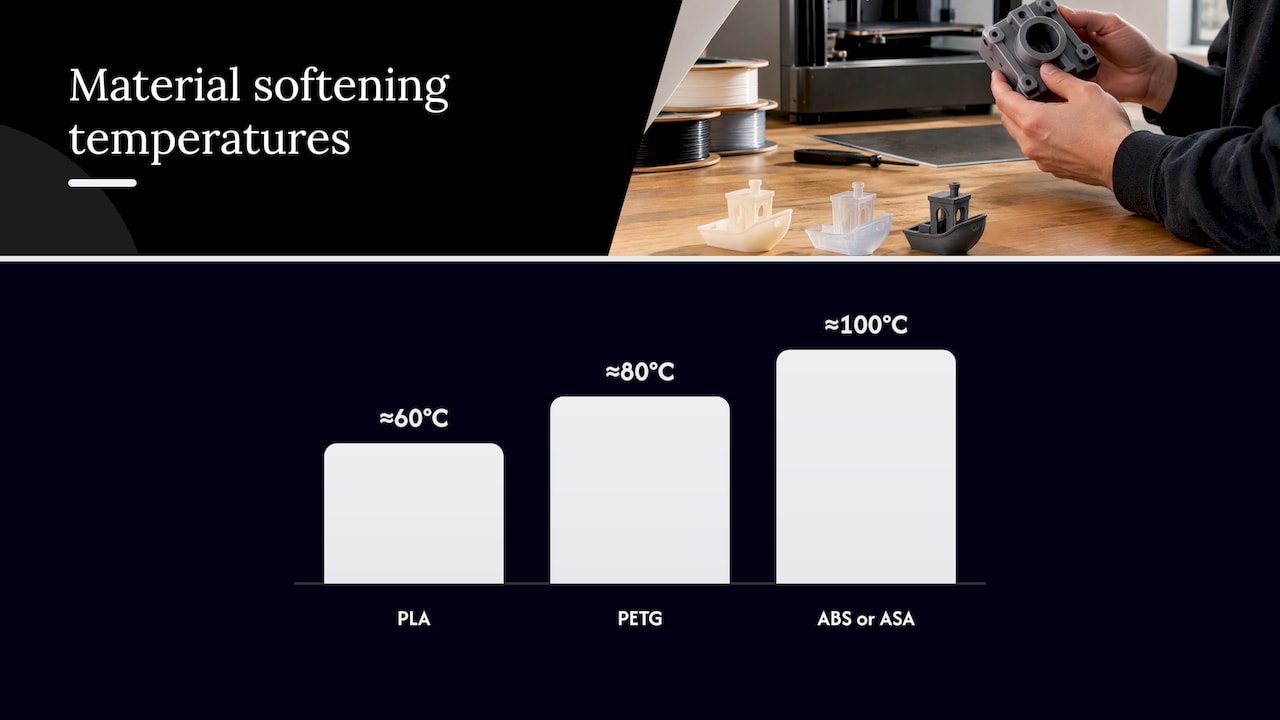
  • Pick the material from the environment: PLA softens near 60°C, PETG near 80°C, ABS and ASA near 100°C, and carbon-fiber nylon is the stiff option for jigs and fixtures.
  • Consistent batches come from a locked print profile, a test print, a defined inspection plan and scan or caliper checks on sample parts.
  • At thousands of simple parts, injection molding usually wins on per-part cost. Below that, FDM avoids tooling and lets you revise the design.

Table of Contents

What small-batch FDM production actually is

There are three stages of making a product, and FDM sits in the middle one.

  1. Prototyping: one to a few parts, built to test fit, form or function. The design is expected to change.
  2. Small-batch (bridge) production: real parts that ship to customers or go into machines, in counts from tens to several hundred or more, before you commit to expensive tooling.
  3. Mass production: large runs where a mold or fixture is paid for up front and earned back through a low price per part.

FDM is the most common way to cover stage two with plastic. Altair’s guide to FDM for end-use parts describes bridge production as an interim step between prototyping and full production in which FDM needs no tooling and builds parts in hours instead of the weeks or months a tool can take. Its stated best-fit profile is useful as a screening checklist:

Screening question Best-fit range for FDM
Quantity 1 to 1,000+ parts
Part size Under about 300 mm (12 in) per side
Material Thermoplastics rated under about 200°C (390°F)
Tolerance Looser than about ±0.13 mm (0.005 in)
Timeline Days to weeks
Design Custom, configured-to-order or still evolving

If your part passes that table, a small-batch FDM run is a reasonable plan. If it fails on more than one line, read the section on when to choose another process below.

Who gets the most from a small FDM batch

The buyers we work with fall into a few groups, and each uses batches differently.

  • Product developers and inventors run 25 to a few hundred units for pilot customers, field trials or pre-sales, while the design is still being refined. Changing a file costs nothing, while changing a mold does not.
  • Small manufacturers make low-volume components such as housings, brackets, covers, spacers, jigs and fixtures that do not justify tooling.
  • Automotive shops and restorers reproduce discontinued trim pieces, clips, brackets and interior parts. For those jobs the batch often starts with a 3D scan of the original part, followed by CAD, followed by printing. We offer professional handheld 3D scanning with accuracy to about 0.1 mm for this work, and scan-to-CAD modeling to turn the scan into an editable model.
  • Engineers on the plant floor print assembly aids, gauges and fixtures where an in-house tool shop would be slower.

Design the part for the process, not the other way around

Most problems in a small batch are designed in. They get multiplied by the quantity. Five rules prevent the common ones.

Choose build orientation first

FDM parts are anisotropic: they are strongest along the printed layers in the X-Y plane and weaker across layers. AlteM’s design guide for FDM says build orientation has to be decided before detailed design for exactly that reason. Orient the main load path along the layers, not across them. A clip that snaps in the layer direction is a clip that cracks at the layer line, and in a batch of 200 you will see it 200 times.

Respect minimum features and overhangs

The same guide gives a rule-of-thumb minimum feature size of about 0.016 in (0.4 mm), notes that the minimum wall thickness in the Z direction equals the layer thickness, and treats overhangs at 45° or less from vertical, or gaps of half an inch or less, as self-supporting. Anything beyond that needs supports, which add print time and leave surface marks. Chamfering a horizontal edge to 45° is usually cheaper than supporting it.

Set walls as multiples of the line width

Wall thickness on FDM is built from perimeters, each as wide as the extrusion line set by the nozzle diameter. A wall that is not close to a whole multiple of that width forces the slicer to fill gaps or drop a perimeter. Our guide to wall thickness in 3D printing shows how to size walls for strength and for repeatability across a run.

Add fillets and inserts where the part is loaded

Sharp internal corners concentrate stress and, on large flat bases, encourage warping. A fillet where a wall meets a base spreads the load. For threads that will be assembled and disassembled many times, design a pocket for a brass heat-set insert instead of printing the thread.
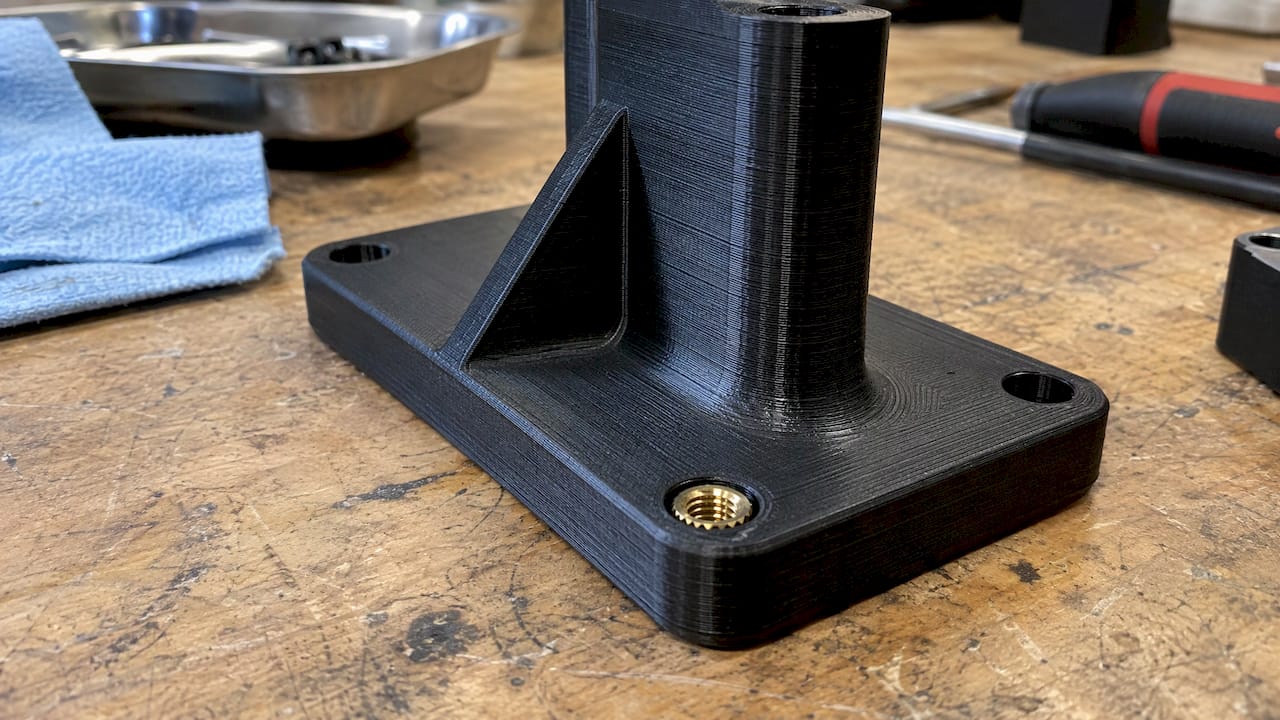
Printed part showing a fillet and brass insert

Tolerance the part honestly

On FDM, the achievable tolerance for most parts is ±0.2–0.5 mm, depending on geometry, size and material. Mating features should include clearance: leave extra gap on press fits and sliding fits, and verify them on a test print. Specifying ±0.05 mm on a printed face invites rejected parts. Where you need tighter control on one feature, tell us at quote time. A better answer than a tighter drawing note is often a design that does not depend on that feature.
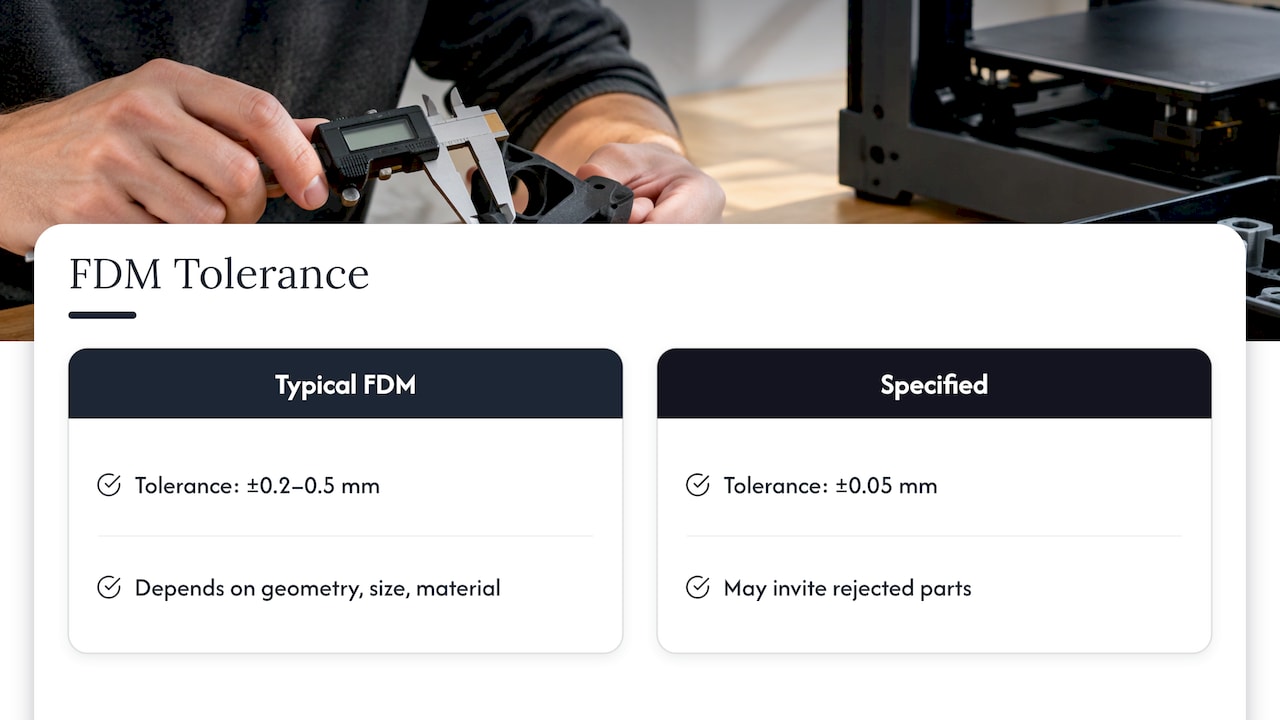
Typical FDM tolerance compared with a tighter specification

Choose the material by the environment

Material choice sets heat resistance, stiffness, UV stability and cost. The glass transition temperature, the point at which a plastic starts to soften, is the number to compare against the worst temperature your part will see. The figures below are typical values for common filament types, so treat them as averages that vary by brand and print settings.

Material Approx. softening temperature Typical use in a batch
PLA ~60°C Visual models, fit checks, indoor display parts
PETG ~80°C Functional parts, enclosures, covers
ABS ~100°C Electronics housings, interior automotive parts
ASA ~100°C Outdoor parts with sun exposure
PC Higher than ABS Brackets that stay hot
Carbon-fiber nylon Higher still Stiff jigs, fixtures, frames

A few notes that matter for production:

  • PETG is a strong default for functional work. A 2026 engineering filament guide describes it as the right starting point for almost every functional print, with good moisture and chemical resistance to fuels, oils and mild acids, where PLA softens at around 55°C.
  • ASA is the pick for parts that live outdoors, because it resists UV. Sunlight is also what fades exterior plastic trim on vehicles, and restorers who already deal with restoring faded plastic trim know how unforgiving long sun exposure is. We cover this further in our guide to materials for outdoor 3D printed parts.
  • Carbon-fiber nylon gives stiffness for jigs, fixtures and frames. SigmaFilament’s framework points out that datasheet strength for these materials varies widely with print orientation and infill, and cites a controlled test in which one 20% carbon-fiber nylon ranged from 22 to 57 MPa depending on infill and build direction. When you specify one, specify orientation as well. Nylons also need to be dried before printing, which the same source puts at 60–70°C for 6–8 hours.

For a head-to-head view of the three most common choices, see PLA vs PETG vs ABS for durable parts. For engineering-grade options, see why filament suits engineering parts.

What drives cost and lead time

In FDM there is no tooling line on the quote, so cost follows machine time, material and labor. Pricing by weight alone misses most of it, which is why we explain in our piece on small batch 3D printing cost why engineers look beyond grams.

The main drivers:

  • Print time per part: height, infill, wall count and layer height all change it. Taller parts and finer layers take longer.
  • Parts per build plate: packing more parts on a plate cuts handling, but a failed plate then costs more.
  • Material: engineering materials cost more per kilogram and often need drying or slower settings.
  • Supports and post-processing: removal, sanding, inserts and assembly are labor.
  • Machine capability: a peer-reviewed cost model for low-to-medium FDM batches treats energy use, which depends on machine size and capabilities, as a key differentiator, and compares cost per piece across lot sizes and materials.

Because these drivers depend on your geometry, we publish no fixed price list. Every production job is quoted individually after a test print of the actual model, and we make no blanket turnaround promises. Two practical ways to lower the quote are to reduce supports through orientation and to relax tolerances on non-critical faces. Our strategies to cut 3D printing costs go deeper.

Keeping a batch consistent

The hardest part of production is not part one. It is part two hundred matching part one. A repeatable process has five pieces.

  1. Lock the file and the profile. Once a test print is approved, the model version, material, orientation, layer height, wall count and infill are fixed. A change of any one is a new revision.
  2. Approve a test print. It exposes warping, fit problems and weak features while only one part has been spent. This is the reason we start every production job there. See engineers, start with one test print for what to check on it.
  3. Define critical dimensions. Mark the few features that must be in tolerance, such as bore diameters, mounting hole spacing and mating faces. Not every dimension needs inspection.
  4. Sample the batch. Measure critical features on parts from the start, middle and end of the run, and across different build plates. Calipers handle simple features. For complex surfaces, a 3D scan compared against the CAD model shows deviation across the entire part rather than at a few points, and our handheld scanning is accurate to about 0.1 mm.
  5. Keep materials dry and consistent. Moisture changes how filament prints, nylon especially. Use one lot of filament for a run where you can.

For runs that need the same result across several batches over months, keeping the profile and the approved sample part on file means a reorder starts from a known baseline.

When another process is the better fit

FDM is a middle-volume tool. It is not the answer to every quantity, and good production planning knows where it stops.

  • Many thousands of simple parts. FDM per-part cost stays relatively flat as quantity rises, while a mold’s cost is spread over every part. Past a few thousand units of a stable design, injection molding generally becomes cheaper per part, even with tooling.
  • Tolerances tighter than ±0.2–0.5 mm on many features, or sealing and glossy cosmetic surfaces, point toward other processes.
  • Temperatures above what thermoplastic filament handles. The Altair guide’s best-fit window ends at thermoplastics rated below about 200°C.

That said, FDM often earns its place even on a path to molding. Printing a pilot batch lets you test with real users, find design flaws and lock the geometry before you invest in a mold. We also print mold masters, so a printed master can serve as a starting point for casting work.

Our perspective on small-batch FDM

We see small-batch FDM as a manufacturing method with its own rules, not as a larger prototype. The rules are that orientation sets strength, walls are built from whole perimeters, and a test print tells you more than a datasheet.

That is why we quote each production job individually after printing your actual model. A batch quoted from a weight estimate can look cheap and then print slowly, warp or fail a fit. A test print answers those questions before they are multiplied.

We run a farm of Bambu Lab printers, so a run can be spread across machines, and we work in PLA, PETG, ABS, ASA, PC and carbon-fiber nylon, with multi-color printing when a part needs it. For automotive shops and restorers, we add handheld scanning and reverse-engineering CAD in the same shop, so an out-of-production part can go from scan to model to printed batch with one contact. We are owner-operated, and you talk directly to the person running your job.

Justin

Start a batch with CC 3D Labs

If you have a CAD file, send it with your material needs, quantity and the dimensions that matter. We will review it, run a test print and quote the batch. If you have only a physical part, we can scan it and rebuild it in CAD first. The overview of what we make is on our services page, and getting a quote for a custom 3D print explains what to include.
CC 3D Labs

Local clients in the Greater Philadelphia area and Bucks County can use residential pickup, since we have no walk-in storefront, and completed orders ship anywhere in the United States. For related reading, see 3D printing on demand for prototypes and custom parts and top tips for low-volume manufacturing.

FAQ

How many parts count as a small batch in FDM?

There is no single cutoff. Altair’s guide treats 1 to 1,000+ parts as the best-fit range for FDM. In practice, tens to a few hundred identical parts is the typical small-batch run. Beyond that, compare against molding once the design is stable.

How accurate are FDM production parts?

Plan on ±0.2–0.5 mm for most parts, depending on size, geometry and material. Accuracy is best on small, simple features and loosens on large, tall or warp-prone parts. Mark your critical dimensions at quote time so they can be checked on the test print and on sample parts from the run.

Which material should I choose for functional end-use parts?

Start with the worst-case environment. PETG (softens near 80°C) suits most functional covers and enclosures, ABS and ASA (near 100°C) suit hotter or outdoor use, and carbon-fiber nylon suits stiff fixtures. PLA (near 60°C) is for parts that stay cool and indoors.

Can you reproduce a part that is no longer made?

Yes, that is a common job for automotive shops and restorers. We scan the original with professional handheld 3D scanning (accuracy to about 0.1 mm), build an editable CAD model, and print the batch. Send details through our scan quote form.

How do I get a quote for a production run?

Send your file, material, quantity and critical dimensions through the 3D print quote form. We quote after a test print of your actual model, so the price reflects the real part. For CAD work, use the 3D modeling and CAD quote form.

Sources

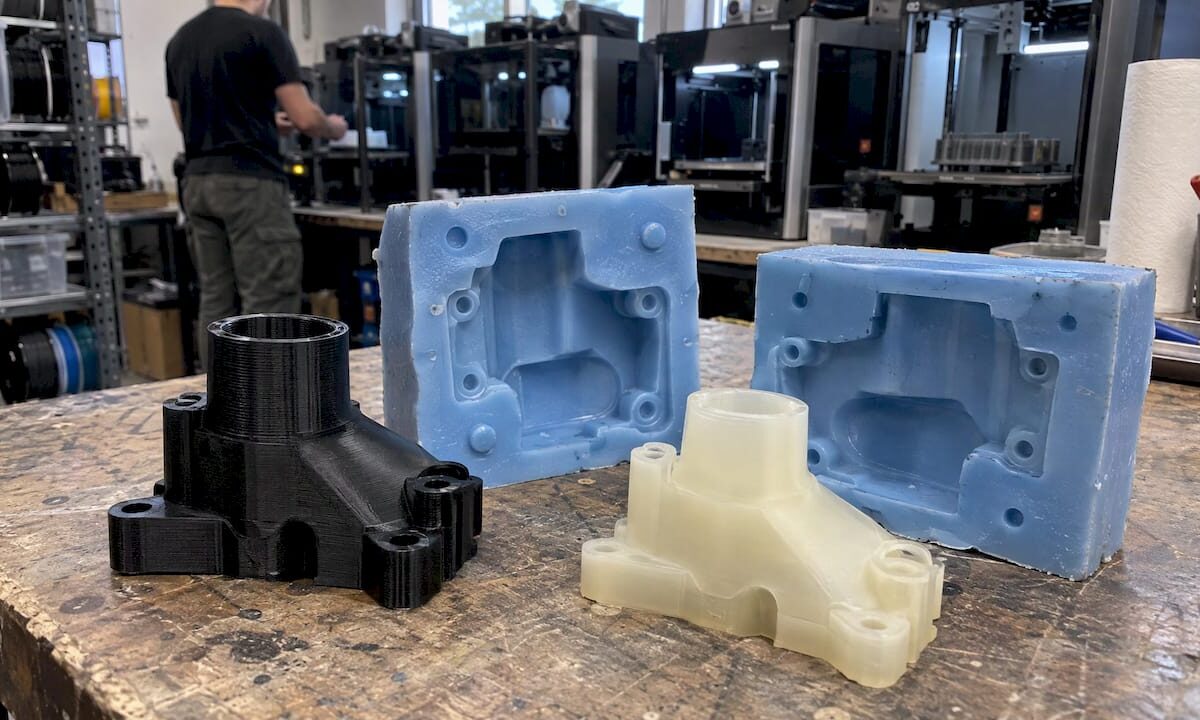
Printed master beside its silicone mold and casting

Silicone Molding With 3D Prints: Masters, Sealing and Casting

Yes, a 3D print makes an excellent master for a silicone mold, and the quality of the mold is decided before any silicone is mixed: by the dimensional accuracy of the master, the way its surface is sealed, and the release agent. We print and finish FDM mold masters at CC 3D Labs, and when the master has to match an existing part, we can start from a professional handheld 3D scan (accuracy to ~0.1 mm) and CAD. This guide walks through the full process for engineers, product developers and small-batch buyers, including the points where molds fail.

CC 3D Labs
cc3dlabs.com
Get a Printed Master for Your Mold
CC 3D Labs prints mold masters and offers scanning and CAD services when your design needs to match an existing part.

Visit

TL;DR

  • A silicone mold is cast around a rigid master. A 3D-printed FDM master works well if its surface is sealed and a release agent is applied first.
  • Printed FDM parts are porous at the layer lines, so silicone can grip them mechanically. Sealing and releasing the master prevents this.
  • Use platinum-cure (addition-cure) silicone, keep sulfur, tin, latex and amine contaminants away from the master, and degas the mix to avoid bubbles.
  • FDM masters typically hold about ±0.2–0.5 mm, so design the master with the final casting tolerance in mind.
  • We quote every master individually after a test print of your actual model. Start at cc3dlabs.com/3d-print-quote/.

Table of Contents

How silicone molding with a 3D print works

The principle is simple. You build a containment box around a rigid master, pour liquid silicone over it, let the silicone cure, and remove the master. What remains is a flexible negative. You then fill that cavity with a casting material such as urethane resin, wax, plaster or cement, and demold the copy.

There are two common ways a 3D print enters this workflow:

  1. The print is the master (the positive). The silicone captures its shape. This is the classic route, and the one this guide focuses on. Smooth-On demonstrates it with an extruded PLA part and a platinum-cure silicone.
  2. The print is the mold box or shell. A printed housing holds the master and the liquid silicone, so the box is disposable or reusable tooling and the silicone becomes the real mold.

You can also print molds directly for casting, but silicone itself is a poor fit for printing: silicone printers exist, but the technology is still niche and the results are typically too soft for many practical uses. For production-quality flexible molds, casting silicone around a printed master remains the standard approach. Our own guide to manufacturing-grade 3D printing covers what makes a printed part suitable as production tooling.

Why a printed master suits low-volume work

A silicone mold is the usual bridge between a one-off prototype and a small batch. Machined steel tooling is justified when you need thousands of parts. When you need ten, fifty or a few hundred copies of a part in urethane or another castable material, a printed master plus silicone is a practical route, because the master can be revised in CAD and reprinted when the design changes.

This is where the master’s accuracy matters most. A silicone mold reproduces whatever it touches: the shape, the layer lines, the blobs and the tool marks. If the master is off by 0.3 mm, every casting is off by roughly the same amount. Our tips for low-volume manufacturing with 3D printing explain how to plan a batch around that tolerance.

Step 1: Get the master right

Choose the print material by what it will face

For an FDM master, the material matters less for the silicone itself than for what the master endures: heat if you accelerate the cure, handling, sanding and release coating. Typical heat resistance, as industry averages, is about 60°C for PLA, 80°C for PETG and 100°C for ABS and ASA. If you plan to warm the silicone to shorten the cure, choose a material that stays rigid at that temperature. Our PLA vs PETG vs ABS comparison goes through the trade-offs, and our guide to annealing explains how to improve heat resistance without warping the part.

Design for the tolerance you need

FDM printing typically holds roughly ±0.2–0.5 mm, depending on geometry and size. Silicone itself shrinks very little: a Shin-Etsu technical data sheet for an addition-curing moldmaking silicone lists linear shrinkage below 0.10% after a 24-hour cure at 25 °C. That means the master’s accuracy, not the silicone, usually sets your dimensional error. If you need a master that matches an existing part, we can scan it, build the CAD model and print the master from that model.

Plan parting lines and draft

Orient the master so the casting can leave the mold without being locked in by undercuts. Silicone flexes, so moderate undercuts release, but sharp ones tear the mold over repeated use. If the master needs a two-part mold, add registration keys, such as divots and channels, so the halves align the same way every time. Design these features in CAD rather than improvising with clay.

Finish the surface

The mold copies everything. Layer lines, stringing and tiny pits will be on every casting unless you remove them. Sand, fill and prime the master to the finish you want in the cast part. Our overview of 3D print finishes lists the options, from sanding to coatings.

Pro Tip: Finish the master one grade finer than you think you need. Silicone captures detail that is barely visible on the bench.

Step 2: Seal the master and apply release

This is the step where most first attempts fail. Silicone generally does not stick to much, but porous surfaces with texture are the exception. Polytek’s guidance on preventing adhesion says porous, deeply textured surfaces can be tricky and suggests sealing them with a PVA solution, a sealer/release such as Pol-Ease 2350, or petroleum jelly.

FDM prints are porous at the layer lines, so the same logic applies. Smooth-On’s sealer and release agent reference guide says porous materials need to be sealed and then released, while nonporous materials need only a release agent, and it lists a print coating and a release agent for FDM, ABS and PLA masters.

A practical order of operations:

  1. Remove supports completely and clean the surface. Dust and residue transfer to the mold.
  2. Sand and fill defects you do not want replicated.
  3. Seal the surface with a coating suited to 3D prints.
  4. Let the coating dry fully before moving on. Wet coatings can interfere with the silicone.
  5. Apply release agent in a thin, even layer to the master and to any inside walls of the containment box.

The release agent matters wherever two materials touch: the master, the box walls and any inserts you plan to remove later. Polytek also notes silicones can stick to glass and some metals, so a flat glass base needs release too.

Step 3: Build the containment box

The box holds the liquid silicone in place while it cures. It can be printed, made from foam board, or assembled from plastic. A printed box has the advantage of fitting your master exactly, with registration to hold it in position.

Practical sizing rules:

  • Leave enough silicone wall around the master. A common rule is 10–15 mm of clearance on each side, so the mold is thick enough to resist tearing.
  • Make the base watertight. Silicone is thin when liquid and will find any gap under the walls. Seal seams with hot glue or modeling clay.
  • Fix the master to the base so it cannot float or shift when the silicone is poured.
  • Add a pour spout and vents if you will later cast into a closed two-part mold.

To estimate silicone volume, calculate the internal volume of the box in cubic centimeters, subtract the master’s volume, and add about 10% for waste. One cubic centimeter is about one milliliter. Most CAD packages report the master’s volume directly.

Step 4: Choose, mix and degas the silicone

For engineered parts, platinum-cure (addition-cure) silicone is the common choice because of its low shrinkage and clean cure. As an example of typical specifications, Smooth-On’s Mold Star 20T is a translucent Shore 20A platinum silicone mixed 1A:1B by volume, with a 6-minute pot life and a 30-minute cure at room temperature. It is rated for roughly 420 psi tensile strength and 470% elongation at break, with a useful range from -65°F to 450°F. Other silicones cure slower, in the range of hours to a full day, so always follow the product’s own data sheet.

Mixing

  • Measure accurately, by weight where the data sheet allows it, and mix thoroughly for the full stated time.
  • Scrape the sides and bottom of the container, because unmixed material leaves soft or tacky spots in the mold.
  • Mix slowly. Whipping air into the silicone creates bubbles you will have to remove.
  • Work inside the pot life. With a short pot life like the 6 minutes above, have the box, release and master ready before you open the containers.

Degassing and pouring

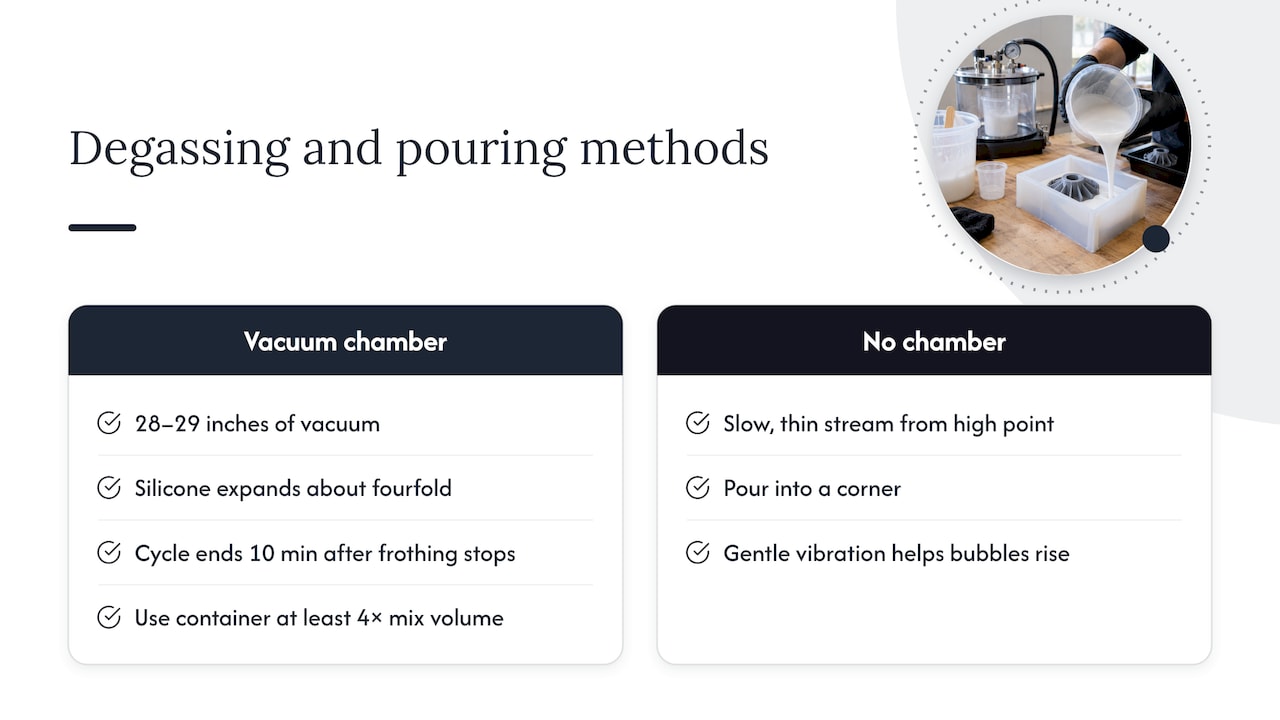
A vacuum chamber removes trapped air. The Shin-Etsu data sheet cited above describes deairing at 28–29 inches of vacuum, with the material expanding about four times in volume while it froths, and the cycle finishing roughly 10 minutes after frothing stops. Use a container at least four times the volume of your mix.

Vacuum degassing and slow-pour silicone methods

Without a vacuum chamber, pour slowly from a high point in a thin stream into a corner of the box, so the silicone climbs over the master rather than trapping air against it. Gentle vibration helps bubbles rise.

Curing

Let the mold cure undisturbed for the full time on the data sheet. If you heat an addition-cure silicone to speed things up, check that the printed master keeps its stiffness at that temperature, which is the reason for the material guidance earlier. Do not demold early to save time: a partially cured mold deforms and tears.

Step 5: Demold and cast

Once the silicone has cured, remove the box walls and cut or peel the mold away from the master. Silicone is flexible, so work slowly and pull from the edges rather than prying at one point. For a two-part mold, the halves separate at the parting line.

Before casting:

  • Inspect the cavity for bubbles, tears and tacky areas.
  • Apply the release agent your casting material requires.
  • Clamp or band the mold halves so the pour cannot force them apart.

Then pour your casting material, whether urethane, wax, plaster or cement, according to its own instructions. For a two-part mold that was built by pouring one half first, clean every trace of clay and spray release before pouring the second half so the silicone does not fuse into one piece.

Why silicone molds fail, and how to prevent it

Problem Typical cause Prevention
Silicone sticks to the master Porous, unsealed FDM surface; no release Seal the print, then apply release agent
Soft, tacky or uncured silicone against the master Cure inhibition from contaminants Keep sulfur, tin, latex, amines away from the master; test a small area
Bubbles on the mold face Air in layer lines or mixed in Seal the master, mix slowly, degas
Layer lines in every casting Unfinished master Sand, fill and prime before molding
Mold tears at demolding Sharp undercuts or thin walls Add draft, leave 10–15 mm of wall
Mold degrades after a few casts Adhesion or wear from the casting material Use release on every cast and match the silicone to the casting material

Cure inhibition

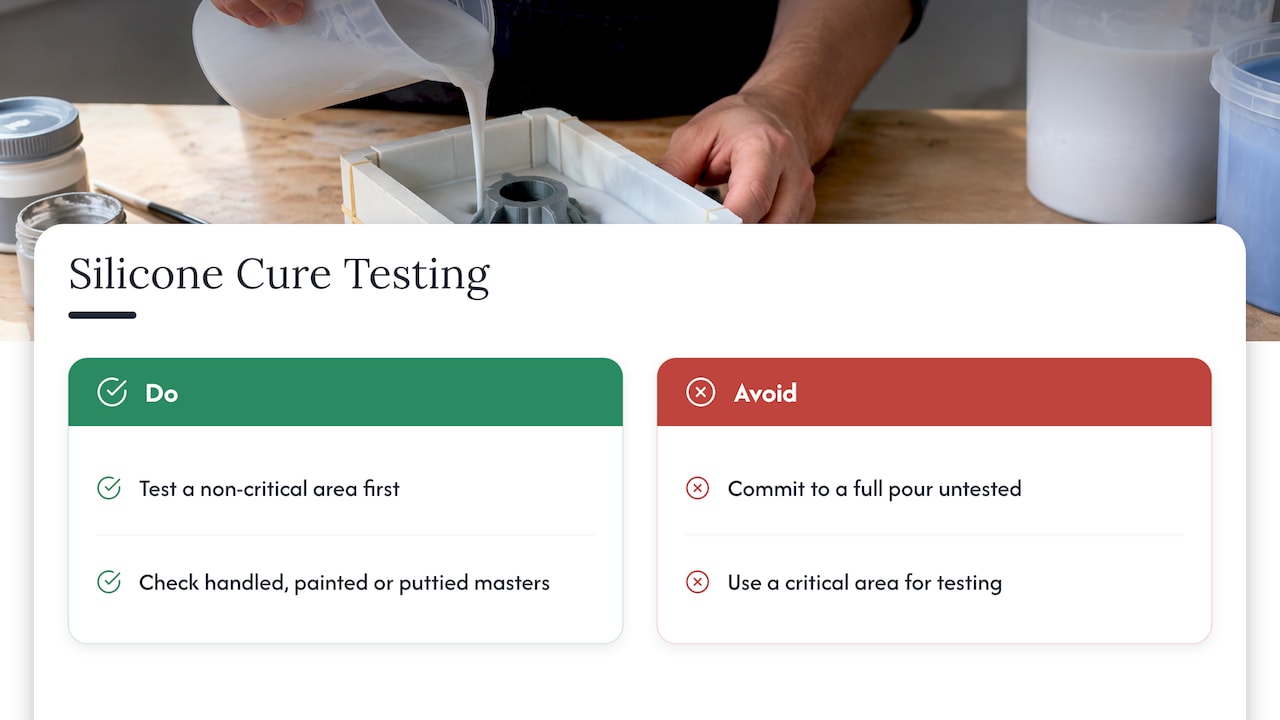
Platinum silicone is sensitive to chemistry. Smooth-On’s product information for Smooth-Sil 950 lists contaminants that can inhibit addition-cure silicone, including latex, tin-cure silicone, sulfur clays, certain wood surfaces and newly cast polyester, epoxy or urethane rubber. It recommends a small test application on a non-critical area before committing to a full pour. The Shin-Etsu data sheet adds sulfur compounds, amines and urethanes, and organo-tin and other organo-metallic compounds. If your master has been handled with gloves containing sulfur, painted, or filled with an unusual putty, test it first. A coin-sized test patch costs a few cents of silicone. A failed full pour costs the silicone, the master and the day.

Cure inhibition

Mold life

A printed master gives you a silicone mold, and the mold’s lifespan depends on the silicone, the casting material and how carefully you release and demold. Treat a first silicone mold as a tool you will remake when it shows wear. Because the master remains in your CAD files, remaking is a matter of reprinting, not rebuilding.

Where a printed master helps most

The process pays off in particular situations:

  • Automotive and restoration parts. Obsolete trim, knobs, gaskets and brackets can be scanned, modeled and printed as masters, then cast in urethane or other materials.
  • Product development. A design that is almost final can be molded in silicone to produce 20 to 50 pre-production parts in a production-like material.
  • Small-batch runs. When the demand is in the dozens rather than thousands, the cost of steel tooling is hard to justify.

Our guide to high-quality scanning for manufacturing describes how a good scan feeds a good master, and the 3D modeling process for businesses shows how scan data turns into editable CAD.

Our approach to mold masters

We run a production farm of Bambu Lab FDM printers and print in PLA, PETG, ABS, ASA, PC and carbon-fiber nylon. We also offer professional handheld 3D scanning (accuracy to ~0.1 mm), scan-to-CAD modeling and printed mold masters. Each job is quoted individually after a test print of your actual model, because the right orientation, material and surface preparation depend on the geometry. Local customers can use residential pickup in the Greater Philadelphia area (there is no storefront), and completed orders ship anywhere in the United States.

If you have a part to reproduce, request a 3D scan quote. If you already have CAD, send it through the 3D print quote form. You can also see everything we do on our services page.

CC 3D Labs

Our perspective

A silicone mold is only as good as the master behind it. We see the master as a precision part in its own right, not a throwaway pattern: its dimensions, its surface and its cleanliness carry straight into every casting.

That is why we build masters from the geometry you actually need. When the part exists already, we scan it with professional handheld 3D scanning (accuracy to ~0.1 mm), model it in CAD and print the master on our Bambu Lab FDM farm. When you design from scratch, we print a test model first and quote the job from what we learn.

The result is a master that is ready for sealing and release, and a clear route from a single prototype to a small batch of cast parts.

Justin

FAQ

Can I use 3D prints to make silicone molds?

Yes. Cast silicone around a rigid printed master inside a containment box, let it cure, and remove the master. FDM prints work well as long as the surface is sealed and a release agent is applied, because the layer lines are porous.

Does silicone stick to PLA?

Silicone generally does not bond to nonporous surfaces, but unsealed PLA is porous at its layer lines, so silicone can grip it mechanically. Smooth-On’s guide recommends a print coating and a release agent for PLA and other FDM masters, applied before the mold rubber.

Can you 3D print with silicone?

Direct silicone printing exists, but it is a specialized technology, and in many cases the parts are too soft for practical use. For most functional parts, engineers print a master in a rigid material, cast a silicone mold around it, and then cast the final part from the mold.

How long does silicone take to cure in a printed mold?

It depends on the product. Some platinum silicones cure in about 30 minutes at room temperature, while others need a full day, as in the Shin-Etsu data sheet’s 24-hour cure at 25 °C. Always follow the data sheet and leave the mold undisturbed for the full time.

How much silicone do I need?

Subtract the master’s volume from the internal volume of your box, both in cubic centimeters, and add about 10% for waste. One cubic centimeter is roughly one milliliter. Your CAD software can report both volumes.

To have a master printed, scanned or modeled, request a quote at cc3dlabs.com/3d-print-quote/, cc3dlabs.com/3d-scan-quote/ or cc3dlabs.com/3d-modeling-cad-quote/.

Sources

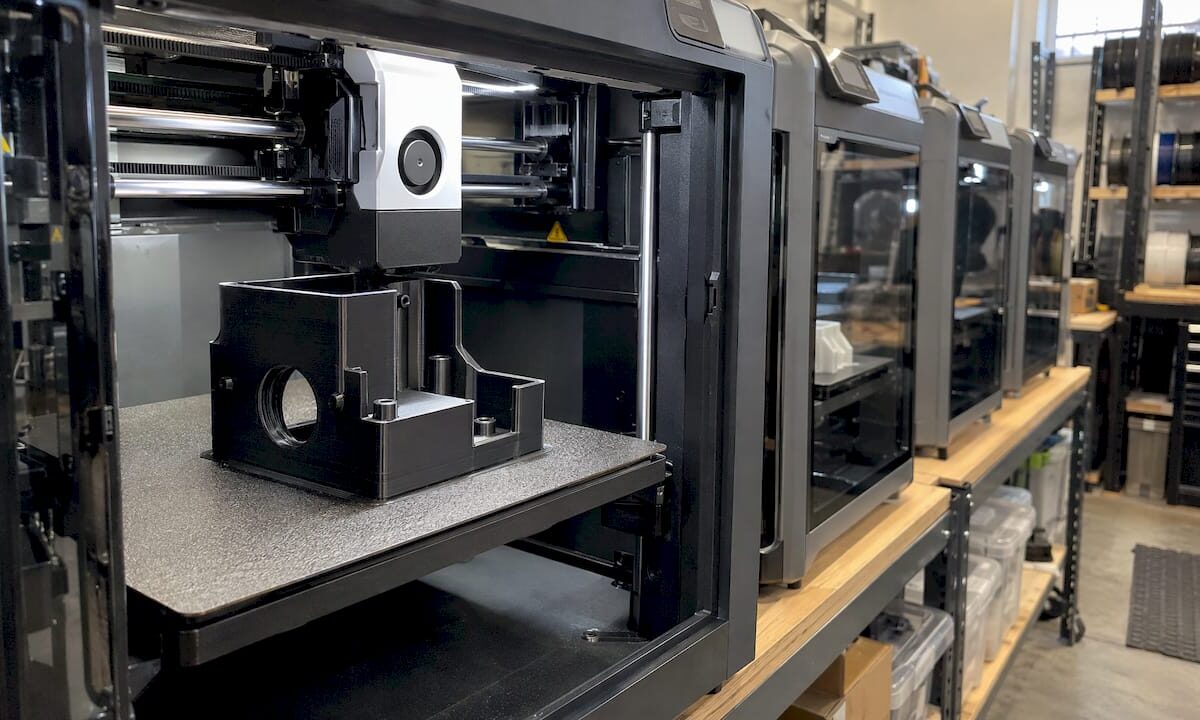
Functional prototype housing printing on an FDM machine

Prototype 3D Printing Cost in Philadelphia and Bucks County

A 3D-printed prototype in the Philadelphia area usually costs somewhere between a few dollars and a few hundred dollars per part, depending on size, material, finish and quantity. The honest answer for any specific part is a quote based on the actual model. At CC 3D Labs, in Bucks County, we publish no fixed price list. Every production job is quoted individually after a test print of your model, so the figure you receive reflects real material use, real print time and the finish your prototype needs.

This guide explains what drives a prototype quote, what industry averages look like, how repeat prints change the price per part, and what to send so the first quote is close to the final one.

CC 3D Labs
Get a Quote for Your Prototype
CC 3D Labs quotes each production job after a test print of your model, with pricing based on your part and requirements.

Visit CC 3D Labs

TL;DR

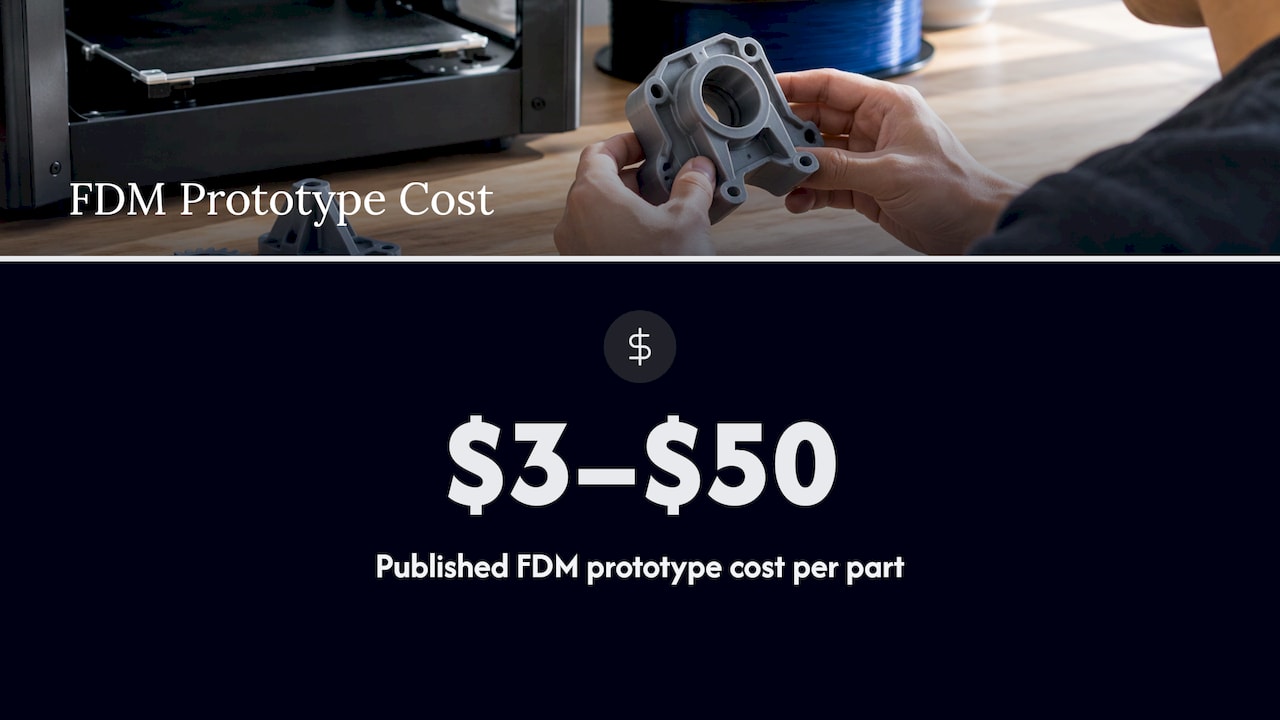
  • Industry averages for FDM prototypes run from about $3 to $50 per part. Your part’s volume, material and finish decide where it lands.
  • Part volume, supports, material, tolerance, finishing and quantity are the main price drivers. Geometry choices you control can move the quote more than any hourly rate.
  • Setup work is spread across a batch, so the price per part usually falls as quantity rises, while material and machine time remain.
  • We quote each job after a test print of your model and make no blanket turnaround promises. Send a STEP or 3MF file, material, quantity and function to get a precise number.

Table of Contents

What a prototype costs: the averages and their limits

Published industry figures give a useful frame, not a quote. One startup-focused guide reports FDM prototypes at roughly $3 to $50 per part, published in March 2026 for the U.S. market. Treat that as an average across many providers and part sizes. A palm-sized bracket in PLA sits near the low end. A large housing in carbon-fiber nylon, printed with supports and finished by hand, can sit well above it.

There is no separate Philadelphia price for 3D printing. Machines, filament and software cost the same here as anywhere in the U.S. What local buyers do get is practical: you can talk to the person running the printers, hand over a physical part for scanning, and collect finished parts by residential pickup instead of paying freight. We have no walk-in storefront, so pickup is arranged per order, and completed orders ship anywhere in the United States.

Bucks County businesses ask what 3D printing typically costs for them. The answer is the same as for Center City: it depends on the part, and a no-obligation quote based on a test print is how you get a real number. The rest of this guide shows how to make that number small and predictable.

What a prototype costs: the averages and their limits

The six factors that set your price

1. Part volume and weight

FDM cost follows material consumed and time on the machine, and both scale with volume. HP’s costing guidance states that larger part volume generally means higher cost. Two parts with the same bounding box can differ by a factor of three in weight if one is a thin-walled enclosure and the other a solid block.

The settings that determine weight are the ones a slicer exposes: wall thickness (set as a number of perimeters multiplied by nozzle diameter), infill density and infill pattern. A prototype that only needs to check form and fit can use light infill. A part that will be clamped, loaded or threaded needs more perimeters and denser infill, and the quote reflects that.

2. Supports and orientation

Overhangs steeper than roughly 45 degrees generally need support material, which adds filament, print time and hand cleanup. HP notes that supports in several additive processes, FDM included, add material and post-processing cost. Orienting the part so that the critical face prints flat against the bed often removes supports and improves surface quality at the same time.

3. Material

Our Bambu Lab farm prints PLA, PETG, ABS, ASA, PC and carbon-fiber nylon. Material choice affects filament cost, print settings and failure risk, and it should follow the job the part has to do.

Material Typical use in prototyping Approximate heat resistance
PLA Form and fit models, presentation parts About 60°C
PETG Functional prototypes, enclosures, tougher parts About 80°C
ABS / ASA Heat-exposed parts, ASA for outdoor and UV exposure About 100°C
PC Stronger, stiffer functional parts See quote discussion
Carbon-fiber nylon Rigid, engineering-grade functional parts See quote discussion

Heat figures are typical material values, not guarantees for a specific print, since orientation and settings change real-world performance. If a prototype will sit on a dashboard, near an engine bay or in a sunlit window, tell us up front so we match the material to the environment. A cheaper material that warps in service costs more than the right one the first time.

4. Tolerance and fit

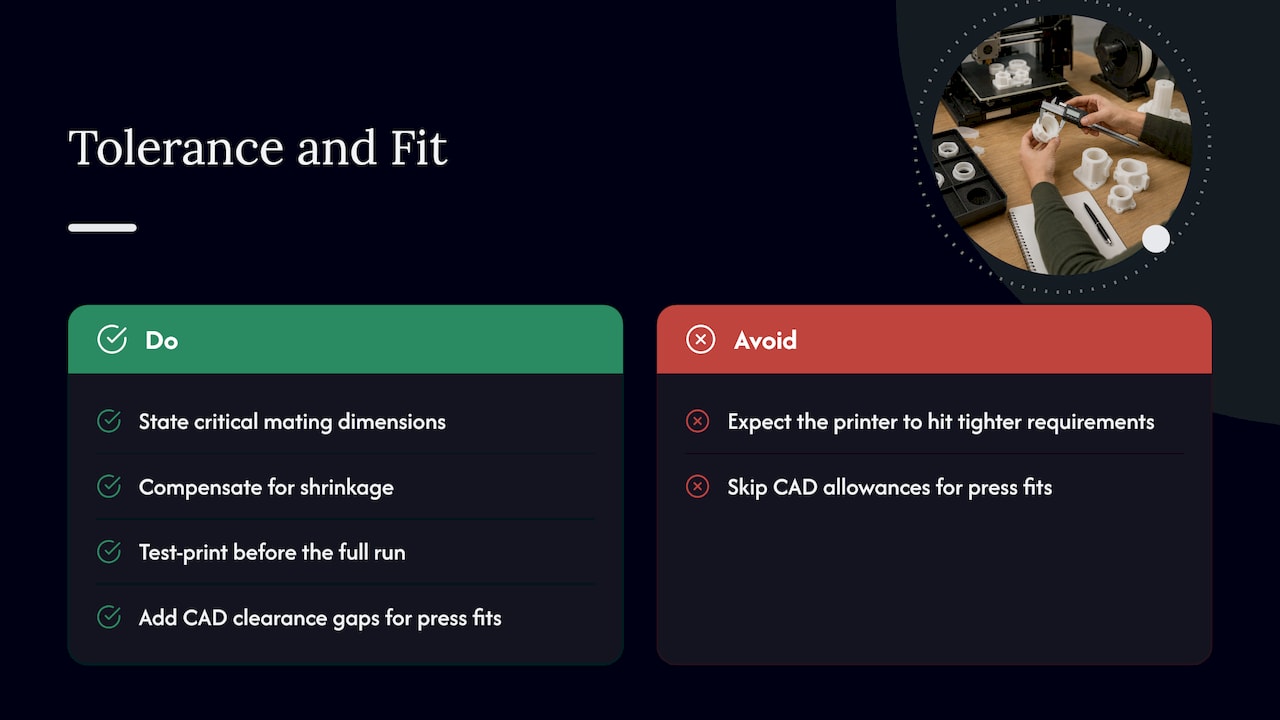
FDM parts typically hold about ±0.2 to 0.5 mm, depending on geometry, size and material. If your prototype mates with another component, state which dimensions are critical. We can compensate for shrinkage on those features, and a test print lets us check them before the full run. Tighter requirements may call for design allowances in the CAD, such as clearance gaps for press fits, rather than expecting the printer to hit a number it cannot.

4. Tolerance and fit

5. Finishing

As-printed FDM parts show layer lines. For a functional prototype that is usually fine. For a part that goes in front of investors or customers, sanding, filling or a different layer height adds labor. Specify the finish you need, not the finish you hope for. A quote that assumes as-printed surfaces will differ from one that assumes a presentation-quality exterior.

6. Quantity

One part carries the entire setup effort: file checking, slicing, plate preparation and the test print. Ten parts share it. The next section shows how much that matters.

How price per part changes with quantity

Setup is a fixed cost, and printing is a recurring one. A published small-batch example from PrintCal assumes $24 of one-off setup and $3.50 of recurring cost per part. At 12 parts, that works out to $5.50 per good part, and at 48 parts $4.00. The setup is shared across more parts, while material, machine time and hand finishing stay constant.

That illustration uses the vendor’s own figures, so read it as arithmetic and not as our pricing. The pattern holds on any FDM farm: the first part is the most expensive per unit, and the curve flattens after a few dozen.

A practical way to use this:

  1. Print one validated part first to confirm fit and function.
  2. Fix any design problems in CAD before ordering more.
  3. Order the next run in a quantity that covers your actual needs for a test cycle, such as 10 to 25, so setup is shared.
  4. Ask for repeat-order quoting once the design is frozen, since the file is already proven.

If you plan to go beyond prototypes, our guide on small batch 3D printing cost covers why engineers look at the whole job and not just grams of filament. For procurement teams who want a framework for comparing quotes, per-unit cost math shows how to separate fixed and recurring costs across suppliers.

What else can appear on a quote

Beyond the printing itself, a prototype quote may include:

  • Design or file repair. If you have a sketch, a mesh with errors or a broken part and no model, CAD work comes first. We offer 3D modeling and CAD services, and if you only have a physical part, we can capture it with professional handheld 3D scanning (accuracy to ~0.1 mm) and build a clean model from the scan.
  • Test print. Every production job starts with one. It is how we confirm dimensions and settings before committing machine time to a run.
  • Finishing. Support removal, sanding or assembly of multi-part prototypes.
  • Shipping or pickup. Local clients can arrange residential pickup. Shipping within the U.S. depends on size, weight and destination.

Ask for these to be itemized. A good quote tells you what you are paying for, so you can decide whether a step is worth it at the prototype stage.

How to prepare a file for an accurate quote

The fastest route to a firm number is a complete request. Quotes slow down when basic details are missing, and each round of questions adds days.

The right file format

For a simple part, an STL or 3MF is usually enough. For a technical part that may need edits, a STEP file helps. A practical comparison of formats says that STL is common and sufficient for many simple prints, while color, multiple materials or tight fit make another format more useful. 3MF carries units, color and multi-material assignments more reliably than STL.

The project details we need

  1. Material, or the conditions it must survive (heat, UV, load, chemicals), so we can recommend one.
  2. Quantity, now and the likely next run.
  3. Critical dimensions and tolerances, marked on a drawing or in a note.
  4. Function: a visual model, a fit check, a working part, a load-bearing part.
  5. Finish: as-printed, sanded, multi-color.
  6. Timeline, with the date you actually need parts in hand. We make no blanket turnaround guarantees, but knowing your deadline lets us plan the schedule honestly. Our note on local 3D printing turnaround explains what affects lead time.

Pro Tip: Add the units to your request and the file name. A part exported in inches and read as millimeters is the most common avoidable error in a first print.

Ways to lower the cost of a prototype

  • Print in stages. Use PLA for early form and fit, then move to PETG, ABS, ASA or nylon for the functional version.
  • Hollow where you can. Lower infill and fewer perimeters on non-structural areas reduce weight and time.
  • Remove supports by design. Chamfers in place of overhangs, and splitting a part so each half prints flat, can eliminate cleanup.
  • Combine variants. If you are testing three versions of a bracket, putting them in one job shares setup.
  • Settle the CAD first. Each design revision after a batch is paid for twice.

Our article on cutting 3D printing costs goes deeper into these tactics for product developers, and choosing the right 3D printing type helps you decide what the prototype stage actually needs.

Our perspective on prototype pricing

We quote every prototype after printing a test of the actual model, and we do it because a per-gram rate hides the things that decide cost: supports, orientation, tolerance on mating features and the finish you need.

Our Bambu Lab farm gives us consistent results across batches, which matters when a prototype turns into ten, then fifty parts. A single wrong dimension repeated across a run is expensive, so we would rather check it on one part first.

We are owner-operated, so you talk to the person who prints your part. We have taken on fragile and complex builds that other shops declined, and we say so plainly when a design needs a change to print well. Many of our automotive and restoration clients start with a scan of an existing part, then move to CAD and printing in the same project.

Our advice: send us the file, the material conditions and the quantity, and let the test print tell you the price.

Justin

Get a quote from CC 3D Labs

If you are a product developer, engineer, automotive shop or small manufacturer in Philadelphia or Bucks County, we can quote 3D printed prototypes and repair parts and on-demand 3D printing and manufacturing for small-batch runs, including engineering-grade materials and multi-color printing.

CC 3D Labs

Our full list of services is on the services page. If you want to understand the steps before you submit, read our guide to getting a quote for a custom 3D print. Ready to go? Request your prototype quote at cc3dlabs.com/3d-print-quote/. For a scan of an existing part, use the 3D scan request form, and for CAD work, the 3D modeling and CAD estimate form.

FAQ

How much does a 3D-printed prototype cost in Philadelphia?

Industry averages put FDM prototypes at roughly $3 to $50 per part, though large, finished or engineering-material parts can exceed that. We publish no fixed pricing. Each job is quoted individually after a test print of your model.

Is 3D printing cheaper in Bucks County than in Philadelphia?

Not in a way you should plan around. Printer time and filament cost the same everywhere, so your quote follows the part, material, finish and quantity. The local benefit is direct communication with the printer operator and pickup without freight.

Does ordering more parts lower the price per part?

Usually, yes. Setup and preparation are shared across the run, as in a published example where cost per good part falls from $5.50 at 12 parts to $4.00 at 48. Material and machine time still apply to every part.

What should I send to get an accurate quote?

Send a STEP or 3MF file (or STL for simple parts), the material or operating conditions, quantity, critical dimensions, finish and the date you need parts. If you only have a physical part, we can scan it and build the model.

Can you ship prototypes outside the Philadelphia area?

Yes. Local customers can use residential pickup, and completed orders ship anywhere in the United States.

Sources

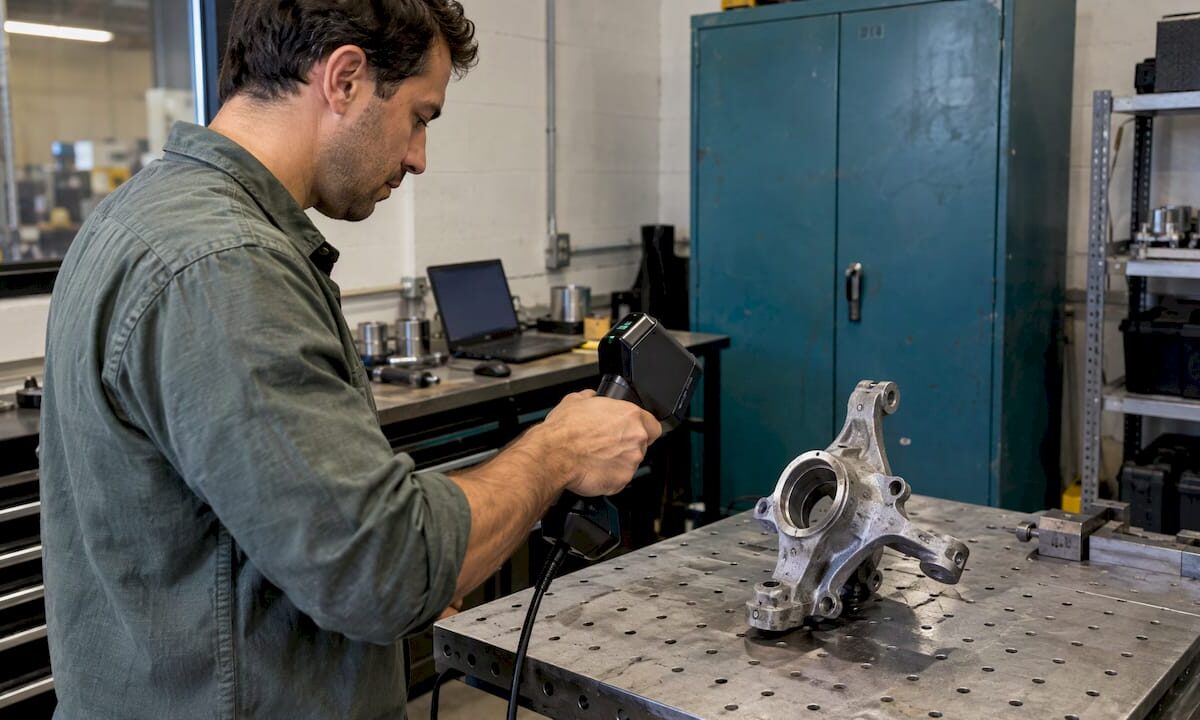
Technician scanning a cast-aluminum steering knuckle

Choosing a 3D Scanning Service: A Buyer’s Guide

The right 3D scanning service is the one whose scanning method, stated accuracy, deliverable files and downstream CAD capability match what you plan to do with the data. Price matters, but it only means something once those four things line up. This guide walks through how to evaluate a provider for a reverse-engineering, part reproduction or prototyping project, what to put in your request, and how to read the answers you get back.

CC 3D Labs
cc3dlabs.com
Turn Scans Into Usable CAD
CC 3D Labs offers handheld 3D scanning for reverse engineering and part reproduction, with scan-to-CAD modeling and CAD design services.

Explore 3D scanning services

TL;DR

  • Define the end use first: inspection and reverse engineering need far tighter accuracy than visualization or archiving.
  • Ask for accuracy in terms of the size of your part, because accuracy typically degrades as the scanned object gets larger.
  • Decide on deliverables before the scan: a raw mesh (STL, OBJ, PLY) is not the same as an editable CAD model (STEP, IGES).
  • Send a clear request with part size, material, surface finish, tolerances and intended use, so quotes are comparable.
  • Choose a provider that can carry the scan through to CAD and, if needed, a printed prototype, so the data never changes hands.

Table of Contents

Start with what the scan is for

Most bad scanning experiences trace back to a mismatch between the job and the method. A scan made to document a part’s appearance is a different product from a scan made to rebuild a bracket that has to fit a discontinued assembly.

Three common end uses:

  1. Reverse engineering or part reproduction. You need dimensional fidelity, clean surfaces and usually a CAD model at the end. This is the most demanding case, and the one automotive restorers and product developers run into most often.
  2. Quality control or inspection. You compare a produced part against its nominal model. Accuracy and repeatability matter most. Our article on scan-based quality control covers how that comparison works.
  3. Design reference or prototyping. You capture an existing object so a new design can wrap around it, such as an enclosure for an existing component. Moderate accuracy is often enough, as long as critical mating features are captured well.

Write one sentence for your project in this form: “We need [deliverable] of [part] accurate enough to [decision it supports].” Every question below is easier to answer once you have that sentence.

Understand accuracy, precision and resolution

Providers use these three terms loosely, and quotes can look equivalent while describing very different results.

  • Resolution is the smallest increment between captured points, usually the point-to-point distance in the mesh. A fine mesh does not make a scan correct.
  • Accuracy is how close the scan is to the true size of the object.
  • Precision is how well repeated measurements agree with each other.

These definitions are consistent across technical explainers, including Artec’s learning center, which also notes that reverse engineering and quality control put more weight on accuracy and precision than visual applications do.

Ask about volumetric accuracy

A single accuracy figure on a spec sheet usually describes a small area under ideal conditions. Aniwaa’s explainer points out that volumetric accuracy, which describes accuracy across several captures, matters more for larger parts, because overall accuracy diminishes as the part grows. It also lists temperature, calibration, operator skill and the manufacturer’s test standard as factors that affect results.

So instead of asking “how accurate are you?”, ask:

  • What accuracy do you expect on a part of my size and shape?
  • How do you handle alignment across multiple scan passes on a large part?
  • Is the figure a manufacturer spec or something you have verified on similar work?

For our own work, we describe it as professional handheld 3D scanning with accuracy to about 0.1 mm. How that translates to a given part depends on its size, geometry and surface, which is why we discuss it per project. Our guide to what handheld scanner accuracy numbers mean goes into the details, and how to optimize scan accuracy covers the variables you control.

Ask how the result is validated

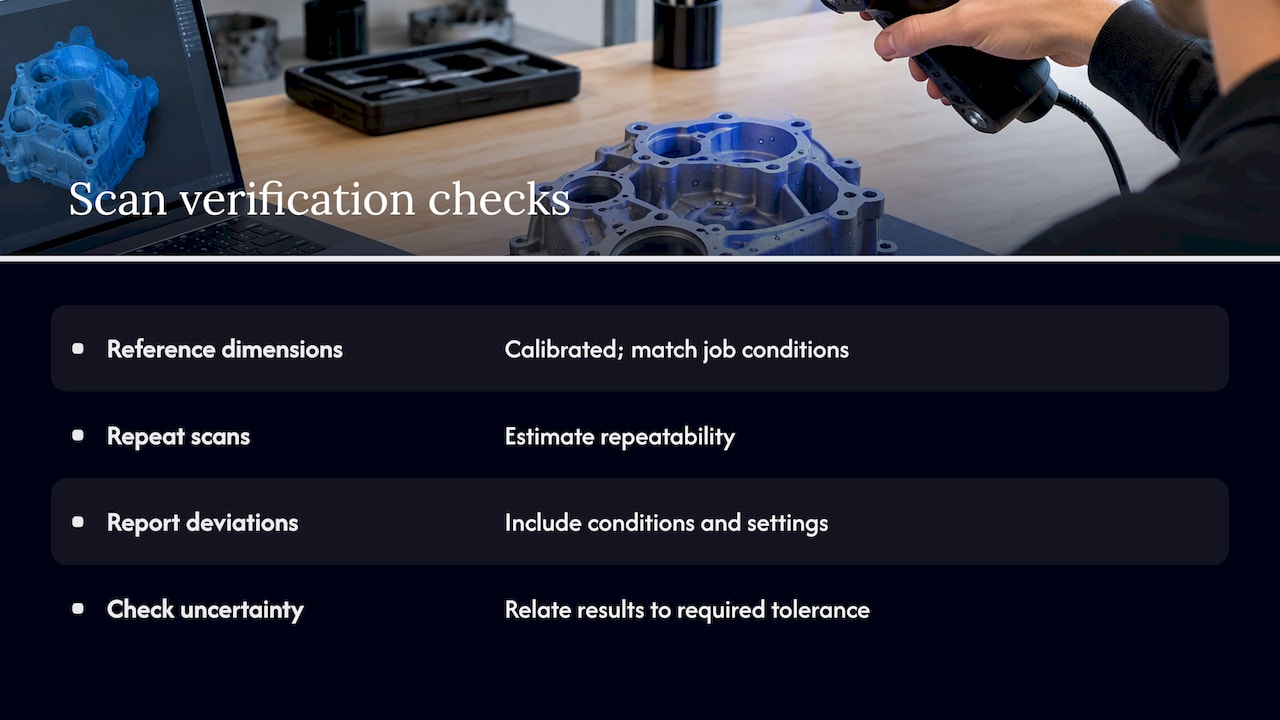
A credible provider can explain how they check a scan. 3DMag’s verification guide recommends validating against calibrated reference dimensions under conditions that match the real job, repeating scans to estimate repeatability, and reporting deviations alongside the conditions and processing settings. The same piece makes a useful point: calibration paperwork is necessary, but it does not on its own show that the uncertainty fits your tolerance. What settles it is whether the provider can relate the measured result to the tolerance you actually need.

Four checks for validating a 3D scan

If your application is demanding, also ask whether the provider works to a recognized standard such as VDI/VDE or ISO for scanner verification, as the Aniwaa explainer suggests. For many reverse-engineering jobs, a documented check of key dimensions against a caliper or micrometer measurement of the original part is the practical test.

Do not over-specify

Tighter is not always better. If you only need an object’s shape to design a fitting enclosure, paying for the highest accuracy tier adds cost without improving the outcome. Match the specification to the decision the scan supports, and put extra budget into the CAD work that follows.

Match the scanning method to the part

Scanning methods differ in what they handle well. Handheld structured-light and laser scanners are flexible: they capture medium-sized parts, complex curves and objects that cannot be moved to a lab. Fixed-position systems and tracked systems trade flexibility for different accuracy profiles.

Practical questions to ask about method:

  • Can the scanner capture the geometry that matters, including deep recesses, thin walls, undercuts and threads?
  • How does the provider deal with shiny, dark or transparent surfaces? These often need a temporary matte coating or careful lighting.
  • Does the scanner use reference targets, and how does the provider keep alignment stable on large or featureless parts?

Automotive parts are a good example. Cast housings, trim pieces, brackets and manifolds combine large smooth areas with small functional features. A good workflow captures the whole shape and then prioritizes the mounting points, bores and mating faces. Our walkthrough of achieving a high-quality scan for manufacturing shows how that is planned.

Decide on deliverables before the scan

The scan itself is only the raw material. What you receive determines what you can do with it.

Deliverable Typical formats Best for Limitation
Raw or cleaned mesh STL, OBJ, PLY Viewing, 3D printing a copy, comparing against a model Not parametric; hard to edit dimensions
Point cloud PLY, other point formats Large-scale capture, software-based inspection Needs processing before most uses
Surface or solid CAD model STEP, IGES Reverse engineering, redesign, manufacturing Requires skilled modeling time
Inspection report PDF, color deviation map Quality control Only as good as the reference model and method

Meshes such as STL, OBJ and PLY can be imported into CAD packages, and reconstructed models are commonly exported as STEP or IGES for use across CAD/CAM tools and manufacturing. If your goal is to change a dimension, add a boss or tune a clearance, a mesh alone will not get you there. You need a rebuilt model.

The step from mesh to editable solid is where much of the effort sits. We explain it in mesh to CAD conversion. For an engineer’s view of the same workflow, this 3D scan to CAD workflow is useful for confirming file compatibility before you commit.

When you request a quote, state the file format you need and the CAD package your team uses. Ask whether the CAD model is delivered as a feature-based model or as a surfaced body, and whether you will receive the original scan data as well. Keeping the raw scan lets you re-verify the CAD model later.

Check whether the provider can finish the job

A scan-only vendor hands you a file and a new problem. A provider that can also model and print lets you validate the result quickly: scan, rebuild, print a test fit, adjust.

This matters for three reasons:

  • Fewer handoffs. The person who understood the scan quality is the person building the model.
  • Faster correction. If a printed test part does not fit, the cause is traced to the scan, the model or the print in one conversation.
  • Better quoting. One provider can describe the whole path rather than leaving you to piece together separate estimates.

At CC 3D Labs, the chain runs from handheld scanning through reverse-engineering CAD to FDM printing on our Bambu Lab farm, with materials including PLA, PETG, ABS, ASA, PC and carbon-fiber nylon. We can also print mold masters from the resulting models. Details on each step are on our services page.

What affects the price and timeline

Scanning is almost always quoted per project, and for good reason. 3DMag’s cost guide lists the factors that make quotes comparable: the required output, tolerance and measurement-uncertainty needs, the size of the object or site, surface and access conditions, onsite logistics, post-processing, and the quality-assurance evidence you want.

In plain terms, two quotes are only comparable if they describe:

  • the same deliverable (mesh versus CAD model),
  • the same accuracy expectation,
  • the same amount of cleanup and modeling,
  • the same documentation.

Be careful with any provider that gives a firm price and date from a one-line email. Part complexity, surface condition and the amount of CAD rebuilding vary enormously. We do not publish fixed pricing or blanket turnaround times for that reason. Each job is quoted individually, and for production printing we base the quote on a test print of your actual model.

How to prepare your request

Good inputs get you accurate quotes and fewer surprises. Include:

  1. Purpose. Reverse engineering, inspection, fit check, reproduction, or design reference.
  2. Part size and weight, plus how many parts.
  3. Material and finish. Glossy, dark, translucent or rubbery surfaces can need extra preparation.
  4. Critical features and tolerances. Mark the dimensions that must be right, such as bore diameters, hole spacing and mating faces.
  5. Deliverable format. Mesh, STEP, inspection report, or all three.
  6. Photos and any drawings. Even a hand sketch with a few measured dimensions helps the modeler.
  7. Delivery method. Local pickup or shipping, and how the part will be returned.
  8. Downstream plan. Will you print it, machine it, or mold it?

Physical preparation helps too. Clean the part of grease, dirt and rust, and flag anything fragile. Our 3D scanning checklist lists the preparation steps in order, and the guide on scanning objects for 3D printing shows how scan choices carry into printing.

Pro Tip: If the part is worn or damaged, send a second, undamaged example if you have one. The modeler can then rebuild the intended geometry rather than the worn one.

Scanning for prototypes: printing or machining?

Many scanning projects end in a prototype, so the process choice comes up. The two common routes are additive (3D printing) and subtractive (CNC machining), and they suit different priorities.

Consideration FDM 3D printing CNC machining
Geometry Internal channels, organic shapes and lattices are practical Shapes must be reachable by a cutting tool
Iteration Design changes mean a new print file Design changes usually mean new toolpaths and setup
Typical tolerance About ±0.2 to 0.5 mm for FDM Generally tighter, depending on machine and material
Materials Engineering thermoplastics for FDM Wide range, including metals

For form, fit and function checks on plastic parts, FDM is well suited, particularly when you expect several design revisions. Material choice matters for heat: PLA softens at roughly 60°C, PETG at about 80°C and ABS or ASA at about 100°C, which are approximate averages and not guarantees for a given part. If a part will sit near an engine bay or a heat source, material selection should be part of the scanning conversation. Our prototyping workflow guide and rapid prototyping overview cover how to sequence these decisions.

A scan-derived CAD model is process-neutral, so the same file can support whichever route your project needs.

Scanning for prototypes: printing or machining?

Questions to ask any provider

Use this list when comparing providers:

  • What accuracy do you expect for a part like mine, and how do you verify it?
  • What formats do I receive, and do I keep the raw scan data?
  • Who builds the CAD model, and how is it checked against the scan?
  • How do you handle shiny or dark surfaces?
  • How is the quote built, and what could change it?
  • Can you print a test part to confirm fit?
  • How do you handle shipping, packaging and return of my original part?
  • What will you tell me if the part is a poor candidate for scanning?

A provider who answers specifically, with reference to your part, is usually one who has done similar work.

Our perspective

We built CC 3D Labs around a simple observation: most scanning problems are really handoff problems. A scan arrives as a mesh, someone else has to rebuild it, and a third party prints it. Each step loses context, and the part that comes back does not fit.

Our approach is to keep the chain short. We scan with professional handheld equipment (accuracy to about 0.1 mm), rebuild the geometry in CAD, and print a test part on our Bambu Lab farm so you can check fit in your hand before committing to a run. We are owner-operated, so you talk to the person doing the work, and we take on awkward jobs, fragile originals and legacy parts that others have turned down.

We also prefer to be plain about what we do not know until we see the part. That is why we quote individually rather than posting a price list. A cast housing and a thin plastic clip are different problems, and the quote should reflect that.

Justin

Start a scanning project with us

CC 3D Labs is a 3D scanning and printing service in the Greater Philadelphia area (Bucks County, PA). Local customers can use residential pickup, since we do not run a walk-in storefront, and finished orders ship anywhere in the United States. We work with automotive shops and restorers, product developers, engineers and small businesses that need scanning, reverse engineering, prototypes or low-volume parts. See our 3D scanning lab for the full scope.

CC 3D Labs

To get a quote, send the details from the checklist above through our 3D scan request form. If you also need printed parts, use the 3D print quote form, and for modeling work, the CAD quote form.

FAQ

Is a mesh file enough, or do I need a CAD model?

A mesh is enough if you want to view the part, compare it against a design or print a copy. If you need to edit dimensions, adjust tolerances or send the part to manufacturing, you need an editable CAD model, typically delivered as STEP. Tell the provider which one you need when you request the quote.

How accurate does my scan need to be?

It depends on the decision the scan supports. Reverse engineering and inspection call for higher accuracy and repeatability than visual capture. Identify the tightest tolerance on your part and ask the provider how they would verify that dimension.

Can a scan be used to 3D print a replacement part?

Yes, in most cases the scan is cleaned, rebuilt into a model and printed in a material chosen for the part’s load and temperature. FDM printing typically holds about ±0.2 to 0.5 mm, so critical mating features are often designed with that in mind. A test print confirms the fit before any larger run.

Why don’t you list prices for scanning?

Cost depends on part size, surface condition, the accuracy you need, the amount of CAD rebuilding and the documentation you want. We quote each job individually so the estimate describes your actual part.

What should I send with my request?

Send the purpose of the scan, part dimensions, material and finish, critical features, the file formats you need and a few photos. Drawings or measurements help. If you can, send an undamaged example of a worn part as well.

Sources